Precision-engineered fitness garments, seamless knit systems, and performance fabrics designed to satisfy strict UK consumer demands for durability, moisture regulation, and compression recovery.
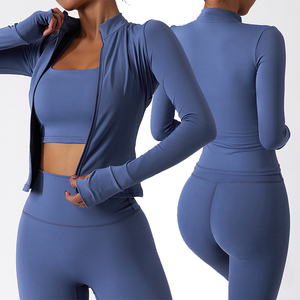
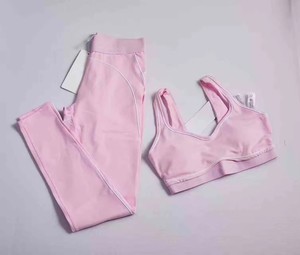
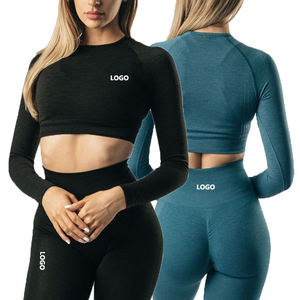
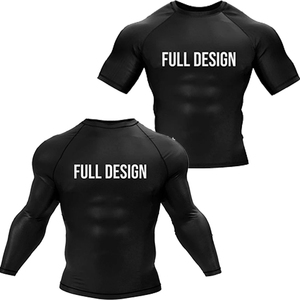
London stands as one of the world's most sophisticated and demanding fitness capitals. From high-density boutique studio chains in the City and Canary Wharf to expansive grassroots football clubs, marathon runners across Hyde Park, and rowing societies along the River Thames, athletic apparel in the Greater London area requires an uncompromising convergence of aesthetic minimalism, anatomical utility, and industrial-grade endurance.
For UK-based fashion brands, independent fitness retailers, corporate merchandising procurement managers, and e-commerce athleisure disruptors, locating trustworthy wholesale sportswear suppliers and exporters requires more than identifying stock off-the-shelf garments. Sourcing directors require vertically integrated manufacturing capability that mitigates global supply chain fragility, complies with strict UK chemical management mandates, and accommodates rapid turnaround cycles.
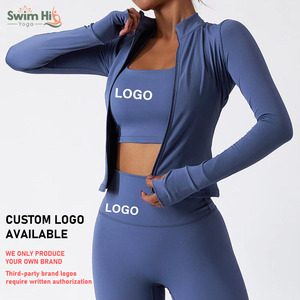
Operating from Sialkot, Pakistan—the globally recognized epicenter of technical sports manufacturing—Verena Sport combines over two decades of export mastery with direct factory-to-door supply chains delivering into London, Manchester, Birmingham, and the broader European market. By bypassing third-party trading intermediaries, London retail buyers access direct-from-mill pricing, comprehensive tech-pack engineering support, and bespoke private label personalization that scales from initial boutique capsule ranges to recurring multi-container distributions.
Technical sportswear is not one-size-fits-all; fabric compositions, breathability coefficients, and seam architectures must be mapped specifically to distinct localized climates, cultural sporting frameworks, and consumer use cases within London and across Great Britain:
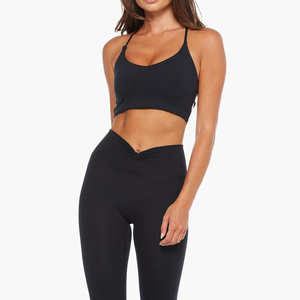
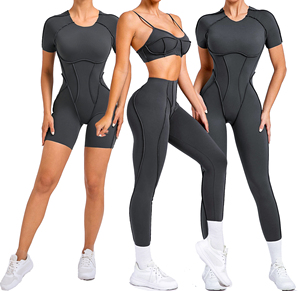
Concentrated in areas like Marylebone, Soho, Shoreditch, and Chelsea, high-end studio brands require four-way stretch leggings and crop tops utilizing 75/25 micro-nylon blends. These garments offer a non-sheer, buttery touch with zero frontal seams, tailored to prevent friction during intense Pilates, Barre, and hot yoga sessions in climate-controlled indoor studios.
With thousands training for the London Marathon and daily Thames Path run clubs, running gear requires moisture-wicking engineered eyelet polyester (140–180 GSM). Essential features include low-profile reflective heat-transfer strips for low-light winter running, flatlock seams to avoid chafing, and water-repellent micro-ripstop windbreakers.
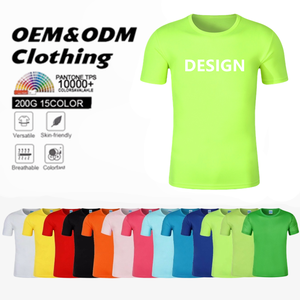
University of London athletic unions, amateur rugby sides, Sunday league football clubs, and rowing teams demand high-tensile 220–260 GSM interlock teamwear. Engineered for hard turf, wet weather, and physical contact, our dye-sublimation process bonds inks molecularly to withstand aggressive weekly wash cycles without fading or cracking.
The post-Brexit British textile retail environment is characterized by acute regulatory compliance scrutiny, growing consumer sensitivity toward ecological credentials, and a definitive pivot toward "commuter-hybrid" performance wear:
British activewear buyers are actively transitioning away from virgin petroleum-based synthetics. London brands are specifying yarns certified by the Global Recycled Standard (GRS), derived from post-consumer recycled polyethylene terephthalate (rPET) bottles and reclaimed ocean nylon. Our factory integrates circular knitting machines capable of processing high-gauge recycled microfibers that match virgin filament yarn in elasticity, hand-feel, and dye-absorption profiles.
Importing sportswear into the United Kingdom requires strict conformity with the UK REACH (Registration, Evaluation, Authorisation and Restriction of Chemicals) regulation and general consumer product safety regimes. Garments must be certified free of harmful aromatic amines, formaldehyde, organotin compounds, and restricted Per- and Polyfluoroalkyl Substances (PFAS) commonly found in legacy water-repellent outerwear. Verena Sport operates under ISO 9001 quality management and manufactures with OEKO-TEX Standard 100 certified fabrics, ensuring every shipment smoothly passes laboratory verification checks upon arrival at British ports.
| Performance Fabric Category | Yarn Density & Composition | Technical Characteristics | Target London Commercial Sector |
|---|---|---|---|
| Pro-Compression Interlock | 280–320 GSM / 75% Nylon, 25% Spandex | Zero-transparency squat proof, 4-way elastic recovery, matte finish | Premium Gymwear, Yoga & Pilates Studio Retailers |
| Hydro-Vapor Tech Mesh | 140–160 GSM / 100% Recycled Poly (GRS) | Pin-hole capillary wicking, rapid evaporative drying, anti-odor finish | Charity Run Events, Marathon Kits & Track Clubs |
| Endurance Thermal Fleece | 300–360 GSM / 80% Cotton, 20% Polyester | Brushed inner loops, pre-shrunk anti-pill finish, dense rib cuffs | Streetwear-Sportswear Hybrid Brands & Lifestyle Retail |
| Sublimated Match-Grade Poly | 200–240 GSM / 100% Interlock High-Filament | High burst pressure, abrasion-resistant, full-bleed digital sublimation | Football, Rugby & Field Hockey Teamwear Clubs |
Drawing on the core manufacturing advantages developed since our founding in 2005 in Sialkot, Pakistan, Verena Sport provides London sourcing directors with a streamlined alternative to complex trading houses:
Pattern-making, CAD grading, laser fabric cutting, flatlock stitching, automated embroidery, continuous sublimation, and custom heat-sealing happen within our company-owned facility. This centralized infrastructure eliminates secondary subcontracting markups and secures end-to-end quality control.
Every consignment undergoes standard AQL 2.5/4.0 inspection protocols. We verify seam tensile strength, colorfastness under wet/dry rubbing, dimensional stability after industrial laundering, and dimensional tolerance accuracy across UK standard sizing scales (XS to 4XL).
We transform tech packs into retail-ready apparel. From custom jacquard woven waistbands, reflective rubberized chest emblems, and recycled silicone logos to FSC-certified custom hangtags and branded biodegradable polybags, we handle total brand packaging in-house.
With sample turnaround times completed in 7 to 10 working days and bulk production delivered in 30 to 45 days, London fashion houses and wholesale distributors can maintain lean inventory levels while responding dynamically to shifting seasonal consumer trends.
Key practical, logistical, and commercial inquiries routinely resolved by our international trade and export division for UK buyers:
Under the UK Developing Countries Trading Scheme (DCTS) / Generalised Scheme of Preferences, Pakistan benefits from preferential trade access to the UK. Many categories of technical sports apparel, cotton knits, and synthetic activewear qualify for reduced or duty-free status into UK ports (subject to commodity code and rules of origin compliance), saving London importers significant landed cost compared to sourcing from non-preferential manufacturing territories.
For high-priority samples and rapid drop-launches, air freight dispatch from Sialkot (via Lahore or Islamabad international freight terminals) directly into London Heathrow (LHR) or London Stansted takes approximately 3 to 6 days. For containerized bulk consignments (FCL or LCL), maritime transport to London Gateway, Felixstowe, or Southampton port averages 22 to 28 days port-to-port on FOB or CIF terms.
Yes. We work from your custom tech packs, size grading charts, and fit specifications. We are experienced in cutting UK-specific grade measurements (UK 6 to UK 22 for womenswear; 36-inch to 50-inch chest grading for menswear), ensuring correct proportions across torso length, inseam drop, and shoulder slopes that match UK consumer fit preferences.
Our sample development loop involves an initial Proto Sample based on your digital vector/tech pack. Once fabric GSM and hand-feel are approved, we issue a Pre-Production (PP) Sample incorporating full branding, care labels, UK-compliant wash symbols, and designated trim hardware. Bulk fabric cutting commences solely upon written PP authorization from your London merchandise team.
MOQs depend on fabric custom-dye requirements and garment complexity. For existing mill stock performance fabrics, flexible production runs start from as low as 100 to 200 units per colorway/style across mixed sizes. For custom lab-dip Pantone dyed or engineered jacquard elastic ranges, standard commercial batches generally start at 300 to 500 units per design.
All bulk knit materials are batched alongside OEKO-TEX Standard 100 certificates and material safety data sheets (MSDS). On buyer request, we coordinate third-party testing with accredited international agencies (SGS, Intertek, or Bureau Veritas) to verify colorfastness to light, perspiration, wash retention, and zero hazardous substance presence before dispatch.
Connect directly with our dedicated export merchandisers. Whether you are expanding an established UK activewear retail chain or prototyping a new performance collection for the London market, we provide direct factory pricing, tech-pack guidance, and expedited sample prototyping.
Inquire Now