Tested across demanding atmospheric conditions, rigorous athletic training routines, and precision UK sizing metrics. Manufactured vertically under single-roof operational oversight.
A rigorous examination of textile physics, unpredictable microclimates, and UK consumer expectations that determine commercial viability in the British activewear market.
Navigating the United Kingdom athletic apparel industry requires far more than applying logos to generic blanks. The UK sports and fitness landscape is heavily shaped by distinct climatic conditions—from damp, blustery mornings across Yorkshire moors to high-humidity boutique fitness environments across London. Sourcing managers and brand founders often fall into the trap of ordering standard 200 GSM polyester garments designed for warm, dry regions, only to face immediate returns due to poor thermal regulation, fabric waterlogging, and insufficient seam abrasion resistance. As a vertically integrated OEM factory, our technical lines are formulated around cross-sectional microfiber filament structures engineered to maintain hydrostatic resistance while facilitating micro-pore capillary moisture diffusion.
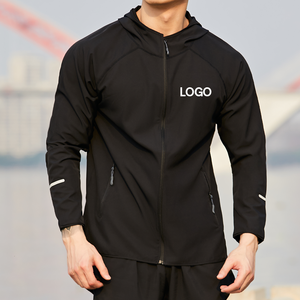
British athletes require multi-functional gear that handles abrupt shifts between drizzle, damp wind, and intense indoor metabolic heat. Our windbreakers and running outer-layers combine lightweight DWR (Durable Water Repellent) finishes with laser-perforated sub-arm ventilation grids to balance weather shedding with rapid evaporative cooling.
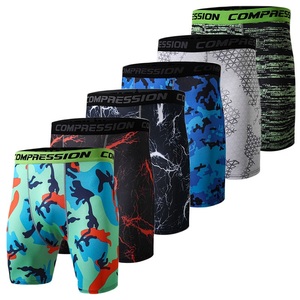
With massive UK participation in Parkrun, Half-Marathons, and nationwide trail networks, compression baselayers and running tights demand 400-needle interlock knitting. This eliminates chafing across 20+ kilometer sessions, incorporates 360-degree Scotchlite-grade reflective visibility, and resists high abrasion cycles on damp roads.
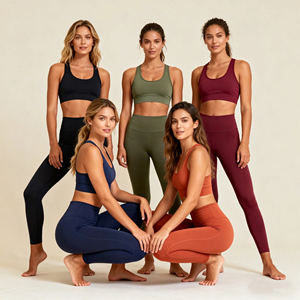
The explosive rise of functional fitness and boutique reformer studios in the UK demands opaque, 100% squat-proof female leggings and high-tensile male gym shorts. We utilize high-gauge nylon-spandex interlocks tested under extreme multi-directional tensile forces to ensure zero transparency under harsh overhead gym downlights.
Furthermore, British sizing paradigms diverge substantially from standard Asian or American patterns. A medium in international fast-fashion frequently fails UK physical testing across chest drop, torso length, and calf compression ratios. Our computerized CAD pattern systems utilize specialized UK grading curves. This guarantees your private label brand delivers an authentic British ergonomic fit straight out of our certified Sialkot export facility, eliminating the cost prohibitive fit-adjustment loops and customer dissatisfaction typical of non-specialist manufacturing partners.
Concentrated regional industrial mastery combined with direct factory-floor control eliminates middleman trading margins and assures end-to-end production governance.
Pattern CAD drafting, computerized laser fabric cutting, flatlock stitching, automated embroidery, high-definition screen printing, and sublimation transfer happen strictly in-house in Sialkot, Punjab.
Full manufacturing compliance conforming with UK REACH environmental directives. Every dye batch and chemical treatment meets certified non-toxic standards, verified through complete inline quality control documentation.
Physical sample creation delivered in 7 to 10 days straight to your UK headquarters. Full production runs are executed in 30 to 45 days, allowing your brand to react swiftly to fast-paced seasonal market shifts.
We supply full-turnkey retail packaging: custom debossed silicone heat seals, woven neck damask labels, organic cotton hangtags, barcode application, and biodegradable polybags designed for immediate UK warehouse intake.
In-depth operational clarification covering tariffs, UK REACH compliance, sample protocols, and cross-border logistics to streamline your overseas procurement process.
We routinely manage export shipments into primary UK entry ports such as Felixstowe, Southampton, and London Gateway, alongside daily air-cargo consolidations directly into Heathrow and Manchester airports. We export on standard FOB, CIF, or DDP terms. Goods originating from Pakistan benefit from the Developing Countries Trading Scheme (DCTS), allowing eligible UK activewear importers to realize significant customs duty reductions when accompanied by our factory-issued proof of origin documentation.
All fabrics used across our private label collections, including our polyester, nylon, and elastane formulations, comply with UK REACH chemical safety parameters. We exclusively deploy OEKO-TEX Standard 100 certified eco-dyes and chemical softeners, ensuring our finished garments are free from restricted azo dyes, phthalates, and per- and polyfluoroalkyl substances (PFAS). Full lab audit certificates and safety data sheets (SDS) are provided directly to your technical compliance team.
Once your team supplies your design tech pack or physical reference garment, our pattern cutters produce computerized 2D/3D CAD mockups. Physical counter-samples are produced, finished with your custom trims, labels, and specified fabric compositions within 7 to 10 working days. Prototypes are then dispatched via express international courier (DHL/FedEx) arriving at your UK office within 3 to 4 business days for fit and physical tensile verification.
Recognizing the balance between inventory risk and unit cost efficiency, our Minimum Order Quantities (MOQs) are structured flexibly across garment categories. Typical minimums begin as low as 50 to 100 pieces per style/colorway for technical sublimation and gymwear collections, scaling seamlessly up to multi-thousand container runs for established retail chains and collegiate sports institutions requiring full bulk production scaling.
