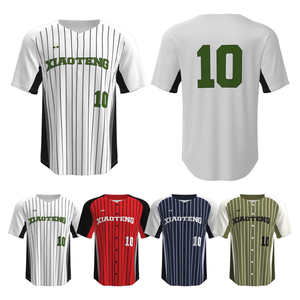
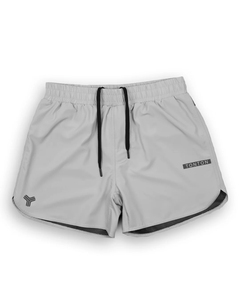
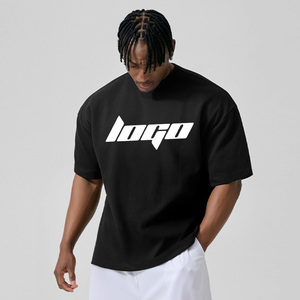
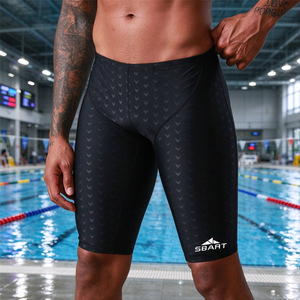
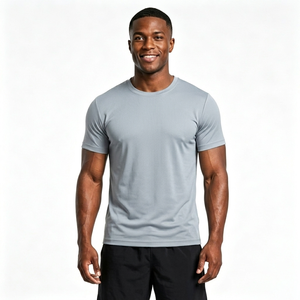
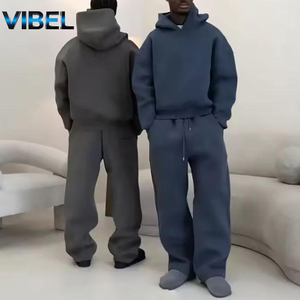
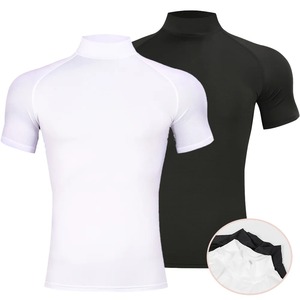
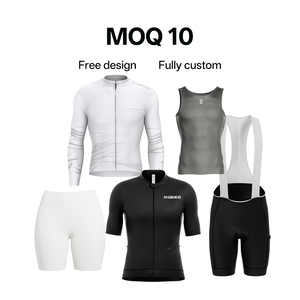
Tested under demanding physical loads, our technical activewear collection leverages flatlock stitching, micro-poly moisture extrusion, and multi-directional compression matrixes suited for Boston's premier sports programs and athletic brands.
A rigorous examination of regional microclimates, collegiate varsity athletics, running culture, and high-performance supply chains across New England.
The Greater Boston metropolitan area and New England regional sports markets present a distinct manufacturing challenge rarely encountered in Southern and Western distribution corridors. With over 65 colleges and universities in the Boston urban perimeter alone, institutional athletic spend is exceptionally concentrated. Procurement officers, collegiate equipment managers, independent fitness brands, and corporate marathon coordinators require apparel capable of enduring intense thermodynamic stress—ranging from damp, below-freezing nor'easter conditions during autumn and winter training on the Charles River, to sweltering, humid summer conditioning sessions.
As experienced custom athletic apparel manufacturers and exporters serving North American supply chains, Verena Sport addresses these regional procurement hurdles through vertical supply line integration. Sourcing directly from Sialkot's globally acknowledged manufacturing hub, we engineer bespoke polyester knit blends, hydrophobic coatings, and mechanical stretch fabrics that conform strictly to NCAA colorfastness standards, NFHS moisture protocols, and consumer-facing retail finishing specifications.
Boston's extensive collegiate athletics require teamwear that bridges extreme physical resilience with crisp institutional branding. We manufacture sublimated jerseys, warm-up tracksuits, and heavy-gauge fleece kits tailored for varsity rowing, lacrosse, hockey conditioning, and basketball teams across Cambridge, Chestnut Hill, and Downtown Boston.
Anchored by the world's most prestigious annual marathon, Boston's running culture demands elite aerodynamic cuts, anti-abrasion inner seams, and micro-mesh ventilation. Our ultralight polyester singlets and running windbreakers prevent thermal drag along Heartbreak Hill and coastal training corridors year-round.
The proliferation of high-end strength conditioning gyms, CrossFit boxes, and combat academies throughout Somerville, South End, and the Seaport District has created massive demand for private label boxy-fit heavy cotton tees, no-gi compression rash guards, and squat-proof functional bottoms that withstand intense chalk, friction, and daily laundering.
Key operational shifts observed by procurement directors, private label founders, and institutional buyers heading into 2025/2026.
| Market Vector | Legacy Sourcing Paradigm | Modern Technical Standard (Verena Sport OEM) | Boston Market Advantage |
|---|---|---|---|
| Fabric Sustainability | Virgin petroleum synthetics, chemical finishes | OEKO-TEX compliant yarns, certified circular polyesters | Aligns with Massachusetts corporate environmental mandates |
| Thermal Adaptability | Single-weight heavy cotton or pure fleece | Multi-tiered base layering, hybrid brushed fleece blends | Withstands New England's volatile shoulder season weather |
| Supply Chain Agility | Rigid 6-month cycles, excessive 3,000 unit MOQs | Agile 7-10 day sample windows, scalable private label runs | Mitigates retail inventory holding costs in high-rent metro hubs |
| Graphic Permanence | Standard plastisol screen prints that crack | Deep dye molecular sublimation & reinforced embroidery | Zero degradation over 100+ commercial wash-and-dry cycles |
Additionally, modern sports merchandisers throughout Massachusetts are shifting rapidly away from intermediary domestic trading agencies that add 30% to 50% markups without physical plant control. Direct factory relationships with ISO 9001-certified overseas manufacturers permit fine-grain oversight over tech pack tolerances, pattern engineering, and custom branding accessories—from customized engraved aglets and rubber heat-seal badges to bespoke barcode polybags ready for third-party logistics (3PL) fulfillment centers across the I-95 logistics spine.
Operating from one of the world's most renowned sporting goods centers, our vertically integrated plant controls every phase of production under one corporate roof.
Zero subcontracting risks. Pattern making, automated fabric laser-cutting, high-density stitching, sublimation, and packaging occur in our dedicated Sialkot facility, ensuring complete quality containment from yarn spool to ocean container.
We maintain strict ISO 9001 quality management procedures and verify OEKO-TEX textile safety, ensuring full audit readiness for American enterprise buyers, NCAA compliance committees, and strict retail environmental specifications.
With more than 20 years dedicated exclusively to global sport textile export, our logistical staff manages all commercial invoices, air/sea freight routing (FOB/CIF), and customs documentation directly for Boston Logan and East Coast seaports.
Comprehensive answers addressing sample lead times, MOQs, tariff logistics, and custom tech pack executions.
We provide full-spectrum CIF and FOB terms to North American ports. Standard express air freight for samples and low-volume production typically clears customs and lands at Boston Logan International Airport (BOS) in 4 to 6 business days. For container-scale bulk orders, ocean shipments route efficiently through the Port of Boston (Conley Terminal) or Port of NY/NJ with fully reconciled US Harmonized Tariff Schedule (HTS) paperwork.
Physical pre-production prototypes and fit samples are fabricated, decorated, and dispatched within 7 to 10 days following digital tech pack confirmation. Bulk production cycles average 30 to 45 days depending on the structural complexity, fabric mill scheduling, and decoration protocols involved.
Yes. We engineer comprehensive white-label and OEM solutions. This includes developing custom dyed pantone fabrics, woven neck labels, laser-cut silicone heat transfers, branded care tags, custom FSC-certified kraft hang tags, barcode stickers, and individualized biodegradable polybags ready for direct inventory intake.
All raw textiles undergo rigorous pre-cut lab inspection. We verify GSM (grams per square meter) weight uniformity, four-way stretch modulus, burst strength, and perform color-matching under D65 artificial light boxes against international Pantone Matching System (PMS) swatches prior to pattern layout cutting.
Unlike rigid industrial conglomerate mills requiring thousands of units per style, our agile manufacturing framework accommodates scalable tiers depending on the specific textile substrate and printing methodology. We assist growing athletic lifestyle brands and specialized varsity programs through structured, tiered trial volumes.
Our in-house apparel engineering department routinely collaborates with sports directors and brand designers. If you lack a comprehensive technical CAD pack, our team can construct complete grading scales, dimensional measurement charts, stitching specifications, and vector placement guides from physical benchmark samples or mockups.
Bridge the gap between visionary athletic design and industrial textile execution. Initiate a technical dialogue with our manufacturing merchandisers today for comprehensive quotes, fabric swatches, and pre-production sampling.