
20+
Years of Specialized Export
10M+
Annual Apparel Units Manufactured
7-10
Days Turnaround on Tech-Pack Samples
ISO 9001
OEKO-TEX Class-1 Compliant Facility
Direct Production Line
Engineered Activewear & Athleisure Solutions for Bulk Sourcing
Tested across thermal comfort thresholds, high-abrasion resilience, and premium colorfastness standards designed specifically for modern performance collections.
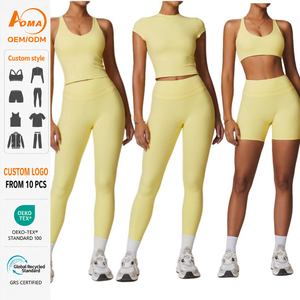
Slim-Fit Contoured Back Yoga & Gym Workout Set
Product Details →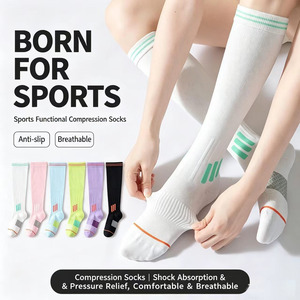
Lightweight Anti-Slip Running Sports Compression Stockings
Product Details →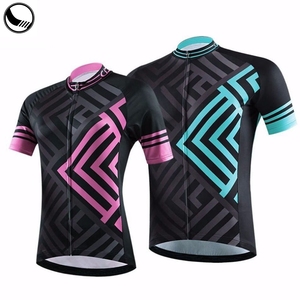
Custom Sublimation Fashion Bicycle & Cycling Uniform
Product Details →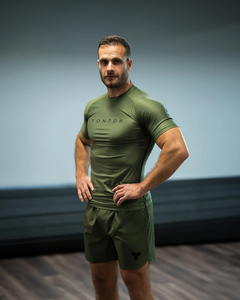
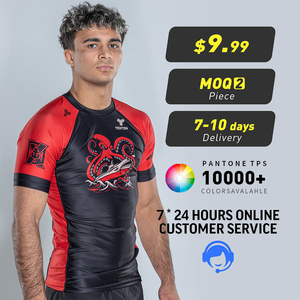
Pro Combat BJJ Rash Guards & Grappling Wear
Product Details →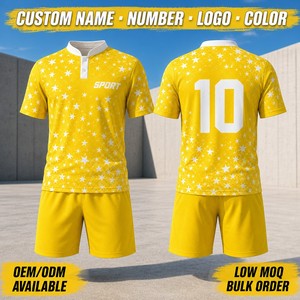
Band Collar Soccer Jersey Teamwear Sublimation Kit
Product Details →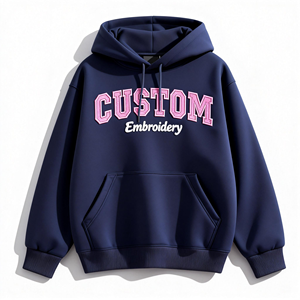
Heavyweight 3D Embroidered Varsity Crewneck & Tracksuit
Product Details →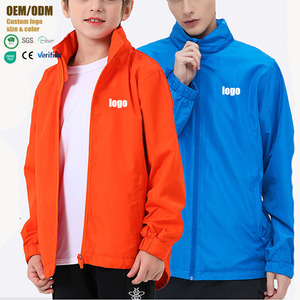
Men's Quick-Drying Athletic Windbreaker & Running Coat
Product Details →The Structural Shift in India's Athleisure and Hybrid Activewear Industry
The Indian sportswear and athleisure segment has transitioned from a specialized, metro-centric gym phenomenon into an expansive everyday lifestyle category valued in multi-billions. As Tier-1 and Tier-2 urban hubs like Bengaluru, Mumbai, Delhi-NCR, Hyderabad, and Pune embrace hybrid workspace models, consumer apparel preferences have pivoted decisively toward garments that deliver seamless transitions from workplace settings to high-intensity functional fitness training. This fundamental demographic trend is pushing national retail chains, standalone fitness labels, and rapidly scaling Direct-to-Consumer (D2C) brands to upgrade their global supply chains.
Procuring athleisure collections for the Indian territory requires an acute appreciation of geographical variables. The subcontinental climate encompasses extremes—from the stifling coastal humidity of Mumbai and Chennai to the severe seasonal variances of Northern India. Consequently, off-the-shelf synthetics procured from low-tier intermediaries inevitably fail, generating excessive returns due to heat retention, fabric discoloration, and poor moisture handling. Verena Sport provides international-grade manufacturing calibrated specifically to overcome these challenges, bridging industrial-scale capacity in Sialkot with precise technical specifications needed to thrive across Indian retail channels.
Fully Integrated Production
Complete in-house operational control covering precision CAD pattern grading, computerized fabric cutting, automated multi-head embroidery, high-definition dye-sublimation, and comprehensive finishing lines under one roof in Sialkot.
Certified Regulatory Quality
ISO 9001 certified quality management operating alongside stringent OEKO-TEX Standard 100 raw materials. Inline inspections ensure that seams, dye resilience, and dimensional shrinkage are verified before bulk customs packaging.
Rapid B2B Turnaround
Agile production lines allowing prototype sample dispatch in 7 to 10 days, followed by streamlined 30 to 45-day commercial bulk container dispatches. Fast-track replenishment prevents seasonal stockouts across prime Indian sales windows.
Performance Optimization Across Indian Commercial & Climatic Scenarios
Manufacturing for the Indian consumer demands technical engineering that addresses localized sweat thresholds, skin sensitivity, and cultural aesthetic expectations. Below are the focal consumer segments currently driving volume sourcing:
Metropolitan Tech-Gyms
Boutique cross-training facilities in Bangalore and Gurgaon requiring 4-way compression nylon-elastane blends that maintain complete opacity (squat-proof) and offer rapid cooling during high-intensity interval routines.
Tropical Coastal Running
Marathon communities in Mumbai and Chennai requiring featherweight 90–110 GSM micro-perforated polyester tops with capillary action to prevent sweat pooling in sustained humidity exceeding 85%.
High-End Corporate D2C
Smart athleisure polo shirts, technical track pants, and tailored jogger silhouettes crafted from combed modal-cotton-poly filaments that allow all-day comfort inside climate-controlled corporate facilities.
Cricket & Team Academies
District and state-level sports clubs demanding high-tenacity sublimated uniforms capable of withstanding extreme abrasive wear, repetitive sliding, and intense sun exposure without structural fiber pill or fading.
| Product Category | Primary Substrate & Yarn Count | Fabric Weight (GSM) | Technical Functional Finishes | Target Application in India |
|---|---|---|---|---|
| MMA / BJJ Rashguards | 82% Poly, 18% Spandex Interlock | 220 – 280 GSM | Anti-Microbial, UPF 50+, 4-Way Stretch | Combat Studios, MMA Dojos, Grappling Clubs |
| Sculpting Yoga Sets | 75% Polyamide (Nylon 6.6), 25% Lycra | 210 – 250 GSM | Peach-Skin Handfeel, Squat-Proof, Zero Chafing | Pilates Studios, Athleisure D2C Brands |
| Compression Stockings | Polyamide / High-Elasticity Spandex | Graduated Pressure | Moisture Barrier, Anti-Slip Silicone Grippers | Ultra-Marathoners, Recovery Lounges |
| Cycling & Track Tops | 100% Micro-Honeycomb Poly | 130 – 160 GSM | Hydrophilic Wicking, Full Sublimation Fastness | Cycling Groups, Triathlons, Club Sports |
| Varsity Crewnecks | 80% Combed Cotton, 20% Poly Terry | 320 – 380 GSM | Pre-Shrunk, 3D Chenille Embroidery, Anti-Pill | North Indian Winter Wear, Lifestyle Chains |
| Performance Windbreakers | 100% Micro-Ripstop Technical Nylon | 80 – 110 GSM | DWR Finish, Windproof Barrier, Packable Shell | Outdoor Trekking, Morning Fitness, Monsoons |
Market Evolution: Where Indian Athleisure Sourcing is Heading (2025–2030)
International brands and domestic Indian enterprises are revamping their procurement models to mitigate geopolitical tariffs and domestic fabric limitations. As India's market matures, three definitive sourcing shifts have emerged:
1. Shift from Pure Cotton to Technical Blended Synthetic Fibers: Historically, India’s domestic garment supply chains relied overwhelmingly on conventional cotton jersey knits. However, cotton retains water, stretches out of shape under strain, and degrades rapidly under repetitive commercial laundering. Contemporary buyers are now pivoting toward high-filament micro-polyester, nylon 6.6, and elastane formulations. Verena Sport’s established supply cluster in Sialkot allows Indian procurement executives to secure specialized synthetic performance textiles that are complex to knit or finish domestically at comparable margins.
2. Micro-Drop Seasonal Releases vs. Massive Inventory Holds: Rapid direct-to-consumer adoption across apps like Myntra, Ajio, and independent Shopify storefronts has forced brands to adopt lean inventory methodologies. Instead of ordering 20,000 units of a single silhouette, sourcing directors favor scalable batch manufacturing (low starting MOQs from 50–100 pieces per style) with swift replenishment channels. Our lean manufacturing cells accommodate iterative drops without compromising unit economics.
3. Demand for Full Private-Label Customization: Modern consumers expect branded aglets, customized waistbands, heat-transfer inner sizing labels, custom woven neck tags, and retail-grade frosted polybags. Sourcing directly from an integrated manufacturer eliminates the cost overhead and timing bottlenecks associated with hiring third-party printers or repackaging houses inside India.
Procurement Guidance
Frequently Asked Questions by Indian Buying Offices & Brands
Key information addressing shipping channels, custom clearance documentation, GST adherence, quality controls, and factory compliance.
How are bulk consignments shipped and cleared into India?
We routinely arrange commercial air-cargo and ocean-freight shipments into primary Indian transport gateways including Nhava Sheva (Mumbai), Chennai, and Air Cargo Complexes at Indira Gandhi International Airport (New Delhi) and Kempegowda (Bengaluru). Full commercial invoices, packing lists with Harmonized System (HS) codes, and Certificates of Origin are furnished to match your customs clearance partner's requirements.
Can you match our Indian demographic size charts and fit profiles?
Yes. International sizing often fails in the domestic Indian marketplace because torso-to-limb ratios and shoulder proportions differ from US/EU fit specifications. We specialize in developing customized grading rules and size curves (covering XS through 5XL) based entirely on your brand's proprietary tech-pack specifications or benchmark reference samples.
What are the standard Minimum Order Quantities (MOQs)?
Recognizing the requirement for agile testing in the growing Indian D2C sector, our starting MOQs for private-label production begin at 50 to 100 pieces per design/colorway for technical athleisure, and as low as 10 pieces for select custom sublimation combat items. Substantial bulk price tiers unlock automatically as your volume expands.
How do you prevent color bleeding during heavy sweat and monsoon washing?
All performance synthetics undergo exhaustive lab dip evaluations, wash-durability cycles (40°C accelerated tests), and Rubbing Colorfastness testing (both dry and wet methods) to Grade 4+ standards. Sublimation uses high-grade Italian dispersion inks that bond molecularly with polyester filaments, preventing bleed, peel, or crack under harsh laundry conditions.
Do you provide sample approval prior to bulk production runs?
Every commercial order commences with a comprehensive sampling process. Within 7 to 10 working days, we fabricate proto-samples based on your tech packs, complete with specified fabric GSM, trims, and branding. Production runs only commence once you test, inspect, and formally sign off on the golden pre-production sample.
What international quality audits and factory standards do you maintain?
Verena Sport operates under strict ISO 9001 certified Quality Management Systems. Our production floor upholds modern safety and labor compliance standards, with OEKO-TEX Standard 100 certified fabrics that guarantee zero toxic dyestuffs, lead, or carcinogenic chemical residues in contact with skin.