Explore benchmark product categories engineered within our vertically integrated Sialkot manufacturing facilities. Every SKU represents strict yarn-to-pack quality governance, precision stitching, and custom private-label readiness.
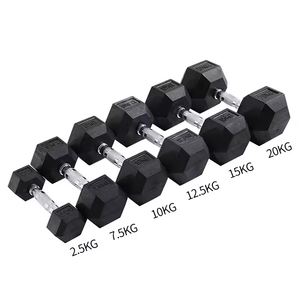
Commercial virgin rubber encased cast-iron core with knurled ergonomic chrome handles. Impact dampening & floor protection engineered for cross-training boxes.
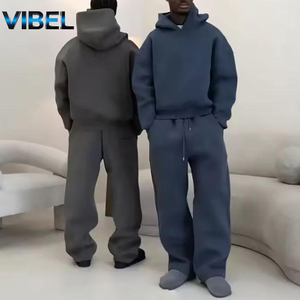
Custom 100% combed cotton or CVC brushed fleece. Drop-shoulder streetwear architecture, dense ribbed cuffs, high-density screen print and puff embroidery options.
Vapor-permeable engineered micro-mesh polyester. Full disperse-dye sublimation ensures zero cracking, zero fading, and maximum heat dispersion during professional match play.
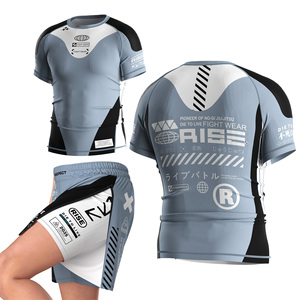
230-260 GSM 85% Polyester / 15% Spandex blend. Reinforced 4-needle 6-thread flatlock seams, anti-microbial fabric treatment, and anti-slip silicone internal waistband.
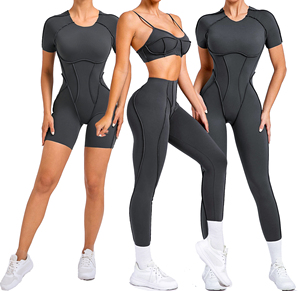
Double-brushed interlocking polyamide elastane. Squat-proof opacity rating, tummy-control contoured high waistband, and moisture-wicking ergonomic cut lines.
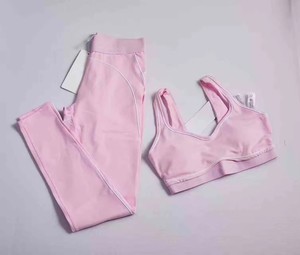
Recycled nylon yarn with high recovery modulus. Structural ribbed side inserts, targeted thermal ventilation, removable molded bra cups, and OEKO-TEX certified dyes.
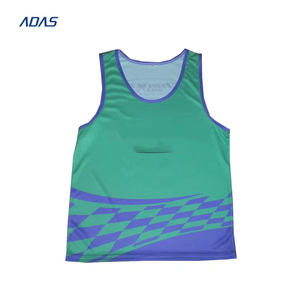
Ultralight 110-125 GSM poly-spandex mesh. Ultrasonic bonded shoulder seams to prevent chafing during long-distance road running. 3M reflective safety transfer accents.
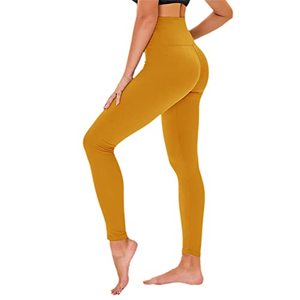
Seamless waistband engineering with hidden back lumbar storage pocket. 4-way stretch mechanical recovery guarantees zero fabric sheer under extreme stretching load tests.
How modern polymer selection, high-gauge knitting tension, and ergonomic seam architecture prevent common garment failure modes in commercial athletics.
In contemporary performance gym clothing, standard carded poly-cotton mixes have been entirely replaced by micro-denier synthetic architectures. Premium athletic wear requires a balance of mechanical tensile elasticity, thermal venting, and permanent colorfastness that survives repetitive high-temperature industrial laundry cycles.
At our factory in Sialkot, we engineer 4-way stretch blends pairing high-recovery spandex (Lycra/elastane) with high-density interlock Polyamide 6.6 or cationic dyeable polyester. The distinction lies in fiber cross-section morphology: trilobal and star-shaped filament cores draw surface perspiration outward via active capillary action, dispersing moisture across an amplified surface area for sub-10-minute evaporation times.
Garment structural integrity during explosive athletic movements—such as deadlifts, Brazilian Jiu-Jitsu grappling, and sprint intervals—depends entirely on thread tension, stitch density, and seam ergonomics. Traditional lockstitch seams rupture under multi-directional lateral pressure; therefore, technical sportswear relies on advanced 4-needle 6-thread flatlock machines (ISO stitch 607).
Furthermore, digital disperse-dye sublimation utilizes pressurized thermal rollers operating at 200°C to 215°C. At this temperature threshold, the synthetic polyester fibers molecularly open, allowing dye polymers to transition directly from gas to solid within the yarn fiber itself. The result is total graphic bonding without stiff hand-feel, pore-clogging, or peeling.
Critical market developments procurement directors, activewear brand founders, and merchandising teams must leverage to mitigate geopolitical risk, tariff shifts, and deadstock vulnerabilities.
Rising tariffs and escalating manufacturing costs across coastal East Asia have accelerated the "China+1" movement. Sialkot, Pakistan, has consolidated its position as the premier international hub for technical activewear and team apparel. Operating within a consolidated ecosystem of local yarn spinners, knitters, and skilled artisans, factories here deliver 20-35% gross cost advantages while meeting ISO compliance benchmarks demanded by top-tier Western enterprises.
The historical model of holding 5,000 units per colorway in warehouse holding facilities is rapidly being superseded by agile, test-and-scale procurement schedules. Modern DTC sportswear labels require flexible manufacturing agreements: starting with low MOQs of 50 to 100 pieces for initial product-market fit tests, followed by rapid 30-day replenishment runs once colorways and cuts are validated by consumer data.
Regulatory frameworks, including the EU Corporate Sustainability Due Diligence Directive and US trade transparency standards, necessitate end-to-end provenance reporting. Global buyers now favor manufacturers capable of furnishing verified certifications for Post-Consumer Recycled (PCR) yarn components, Global Recycled Standard (GRS) documentation, and closed-loop non-toxic dye facility audits.
By unifying pattern drafting, laser cutting, automated sewing, screen printing, embroidery, and final quality assurance under a single corporate roof in Sialkot, we eliminate broker markups and middleman friction.
From yarn inspection and lab dip color matching to final heat-sealed barcoded packaging, our operations remain strictly in-house. This centralized governance preserves exact sizing tolerances, stitch tensions, and aesthetic continuity across repeat seasonal production batches.
Every production batch undergoes inline multi-point inspection and final randomized audits using ANSI/ASQ Z1.4 (ISO 2859-1) AQL 2.5 standards. Dimensional stability, seam pull thresholds, colorfastness under perspiration, and weight GSM tolerances are systematically certified.
We transform conceptual sketches and Adobe Illustrator tech packs into market-ready retail products. Our OEM services include woven neck tags, eco-friendly heat transfer care labels, branded silicone aglets, custom metal zipper pulls, and customized polybags or presentation cartons.
Comprehensive reference matrix detailing machinery, capacities, supported fabric blends, and trade logistics.
| Manufacturing Vector | Factory Capabilities & Specifications | Brand & Buyer Value |
|---|---|---|
| Supported Fabrications | Polyester/Spandex (80/20, 85/15), Nylon 6.6/Spandex, Recycled rPET, Micro-Mesh, Heavyweight French Terry (320-500 GSM), Cotton/Elastane blends, CVC Fleece. | Comprehensive Portfolio Complete range from ultra-breathable running tops to heavy streetwear gym hoodies. |
| Seaming & Assembly Machinery | Yamato & Juki 4-Needle 6-Thread Flatlock, Overlock, Lockstitch, Ultrasonic Bonding, Computerized Bar-Tacking, Double-Needle Coverstitch machines. | Zero Failure Seams Maximum burst pressure tolerance during extreme powerlifting and cross-training movements. |
| Decoration Techniques | Full Disperse-Dye Digital Sublimation, High-Density Screen Printing, 3D Silicone Transfer, Direct-to-Garment (DTG), Puff Printing, 3D Chenille & Flat Embroidery. | Retail Aesthetic Multi-texture decorative freedom matching top global athleisure branding standards. |
| Sampling & Bulk Lead Times | Counter-sample & Proto: 7 to 10 Days. Bulk Production Run: 30 to 45 Days following tech pack approval & lab dip signing. |
Agile Time-to-Market Seasonal drop synchronization ensuring your shelves are stocked on calendar. |
| Compliance & Certifications | ISO 9001:2015 Quality Management Systems, OEKO-TEX Standard 100, SEDEX SMETA Ethical Auditing readiness, GRS (Global Recycled Standard) verified fibers. | Audit Ready Full customs compliance for export across North America, the UK, Europe, and Australasia. |
| Trade Terms & Logistics | Incoterms: FOB (Karachi Port / Sialkot Dry Port), CIF, DDP by Air Express (DHL, FedEx, UPS) and Sea Container Freight. | Seamless Global Freight Flexible incoterms tailored to commercial freight forwarders or direct door deliveries. |
Essential clarifications addressing sampling protocols, custom trims, testing standards, and payment terms for commercial buyers.
Consult directly with our Sialkot manufacturing engineering team. Whether establishing a high-volume private label collection, producing technical sublimated team kits, or optimizing fabric supply chain margins, our vertically integrated plant is equipped to deliver.
