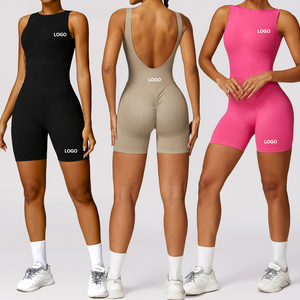
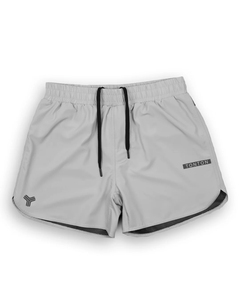
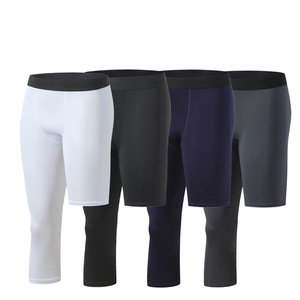
Explore our export-certified activewear, compression wear, and athletic running gear engineered with moisture-wicking textiles, multi-directional stretch, and reinforced stitching.
Over the last decade, professional athletic apparel sourcing has evolved from simple cut-make-trim (CMT) operations into a high-technology, scientifically driven discipline. Today's global sportswear brands, independent fitness labels, and teamwear distributors cannot survive on standard generic jersey knits. Procurement demands high-tenacity yarns, ergonomic zoning, thermal micro-regulation, and non-toxic dye certifications like OEKO-TEX Standard 100.
Modern sports apparel engineering focuses extensively on mechanical elasticity versus elastomer fatigue. While conventional gym wear historically relied on high percentages of elastane that inevitably deteriorated under repetitive sweat exposure, modern Chinese manufacturing hubs leverage high-twist modified nylon and fine denier polyester filatures. These materials provide mechanical recovery without fiber rupture, ensuring that compression tights, BJJ shorts, and yoga jumpsuits retain tensile modulus across 100+ industrial wash cycles.
Hydrophobic inner surfaces engineered alongside hydrophilic outer capillary structures facilitate active liquid moisture transport away from the dermis during maximum cardiac exertion.
Four-needle, six-thread flatlock assembly configured with bulked filament threads prevents seam abrasion on friction contact points while retaining 95% base fabric elongation.
Disperse ink chemistry vaporized directly into polyester matrices under 210°C vacuum platen pressing ensures edge-to-edge color saturation that never cracks, peels, or compromises fabric pore porosity.
Direct vertical integration eliminates intermediary brokerage fees, ensures total traceability from yarn lot to boxed packaging, and secures strict delivery schedules.
In-house pattern digitizing, laser cutting tables, automated computerized sewing lines, full-format sublimation, 3D embroidery machines, and cleanroom packaging units work under centralized management oversight.
Every batch undergoes incoming fabric GSM testing, elasticity recovery index checks, seam shear load testing, 4-5 level colorfastness verification, and independent pre-shipment AQL 2.5 defect audits.
Serving premier sporting clubs, fitness franchises, and retail e-commerce powerhouses across North America, the UK, Europe, Australia, and the Middle East with comprehensive FOB, CIF, and DDP trade clearance documentation.
Our rapid-response sample team reviews technical specifications, grades custom size grading charts from XS through 5XL, generates digital 3D virtual fittings, and outputs physical golden samples within 7-10 business days.
Tailored custom trims including jacquard branded elastic bands, silicone heat-seal transfer logos, woven damask neck labels, custom cardstock hangtags with scannable QR codes, and biodegradable frosted polybags.
No sales agents or non-technical intermediaries. International buyers collaborate directly with English-fluent garment engineers and production merchandisers via live chat, video conferences, and step-by-step progress logging.
Industry forecasts show that performance brands operating in 2025-2030 must pivot their procurement frameworks toward these four mission-critical operational standards.
Wholesale buyers are shifting away from rigid 2,000-piece container orders to agile, iterative drops of 100-300 units per SKU. This preserves operating capital, shortens lead times, and eliminates dead stock obsolescence.
Global retail demand now heavily mandates GRS-certified recycled polyester (rPET) derived from oceanic plastics, as well as bio-based polyamides, accompanied by transparent carbon auditing from yarn to final garment.
Eliminating side seams through computerized round-bed knitting reduces fabric scrap wastage by up to 35% while engineering targeted gradient compression, ventilation zones, and ergonomic body contours.
The boundary between high-intensity performance wear and premium street lifestyle is dissolved. Garments require heavy-weight luxury hand-feel (e.g., 280-320 GSM boxy tees) fused with anti-odor, silver-ion moisture control.
Benchmark engineering tolerances, material composites, and manufacturing parameters across core product lines.
| Product Category | Primary Substrate Options | Typical Fabric Weight | Recommended Seaming | Standard Production MOQ | Optimal Printing / Decoration |
|---|---|---|---|---|---|
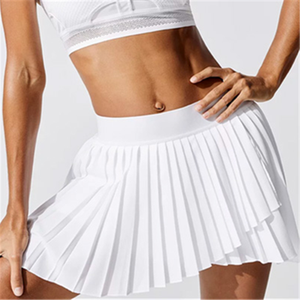
| Pleated Tennis Skirts & Inner Shorts | 85% Polyester / 15% Spandex or 75% Nylon / 25% Spandex | 180 – 220 GSM | Overlock skirt hem, Flatlock liner | 50 – 100 Pcs per color | Silicone heat-transfer, Heat-bonded waistband logo |
| Varsity & Track Crewnecks | 100% French Terry Cotton, 80/20 CVC Brushed Fleece | 360 – 460 GSM | Twin-needle coverstitch, 2x2 Rib collar | 100 Pcs per design | 3D Chenille embroidery, High-density puff screenprint |
| High-Strength Yoga Jumpsuits | 73% Micro-Nylon / 27% Spandex (Brushed Peach Finish) | 220 – 260 GSM | Seamless tubular or 4-Needle 6-Thread | 100 Pcs per color | Reflective 3M transfers, Tonal silicone branding |
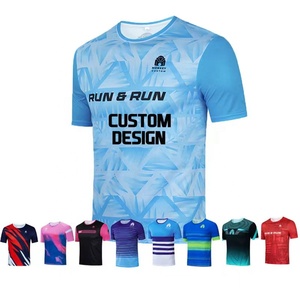
| Sublimated Running Shirts | 100% Micro-Birdseye or Poly Pin-Hole Jacquard | 120 – 145 GSM | Ultrasonic bonded hem or Flatlock seam | 50 Pcs per artwork | All-over digital sublimation (Italian J-Teck inks) |
| Heavyweight Boxy Gym Tees | 100% Combed Compact Cotton / Cotton-Elastane blend | 240 – 280 GSM | Bound rib collar, Drop-shoulder topstitch | 100 Pcs per color | Vintage acid wash, Water-based discharge screenprint |
| BJJ & MMA Compression Shorts | 88% Polyester / 12% Spandex Interlock + Power Mesh | 240 – 280 GSM | Reinforced 6-thread flatseam with bar-tacking | 100 Pcs per style | Gas-permeable sublimation, Jacquard woven elastic |
Direct, technically verified answers addressing contract manufacturing, sampling protocol, quality verification, and international shipping.
Prototyping and golden sample development generally requires 7 to 10 working days following tech pack confirmation and fabric swatch selection. Once the pre-production sample (PPS) receives buyer sign-off, bulk production runs typically take 30 to 45 business days depending on fabric milling lead times, order volume, and decoration complexity.
Yes. While industrial fabric dyeing mills standardly require high poundage per vat, we maintain vast stock inventories of ready-to-cut performance textiles in baseline and seasonal palettes. This lets us support emerging private label brands and niche athletics clubs with initial orders as accessible as 50 to 100 pieces per color/style.
We solve the "squat-proof" transparency challenge through high-gauge interlocking knit construction (minimum 36-gauge circular knits) using dual-core filament yarn at weights not less than 240-260 GSM. All activewear fabrics intended for bottoms undergo back-lit mechanical stretch testing before bulk cut authorization.
Our engineering team works with vector-based Adobe Illustrator (.AI), PDF, or CAD DXF files. Specifications should ideally specify finished flat garment measurements, grading increments, preferred pantone references (TPX/TCX), seam stitch types (e.g., ISO 607 flatlock), and trim placement coordinates.
Every order can be finished with retail-ready branding. We supply custom soft-touch woven neck labels, heat-sealed tagless transfers, embossed hang tags with barcoding, personalized elastic drawcords with engraved metal aglets, and biodegradable ziplock polybags suited for e-commerce fulfillment.
We implement a 4-stage inline inspection matrix: incoming raw material audit, post-cut precision checks, in-line workstation stitching inspection, and 100% final pressing and measurement audits. Garment dimensional tolerances are held within ±1.0 cm according to international export AQL 2.5 standards.
We support standard Incoterms including EXW, FOB (Shanghai/Ningbo/Shenzhen), CIF, and end-to-end DDP (Delivered Duty Paid) air or ocean freight right to your commercial fulfillment warehouse. Full export documentation includes commercial invoices, packing lists, bills of lading, and certificates of origin.
All functional textiles are milled in compliance with OEKO-TEX Standard 100 and REACH chemical limits, ensuring zero hazardous fluorocarbons (PFCs) or formaldehyde. Fabrics achieve Grade 4 to 5 fastness against washing, perspiration, and wet rubbing tests in accordance with ISO 105 protocols.
Submit your tech pack or reference design today. Our engineering and merchandiser team will analyze your specifications, offer fabric optimization insights, provide sample cost projections, and deliver prototypes in 7-10 days.
Send an Inquiry