Engineered for high-intensity court dynamics, rapid thermal displacement, and rigorous multi-season wear. Review our flagship production capabilities spanning custom sublimated jerseys, technical base layers, and compressive training kits.
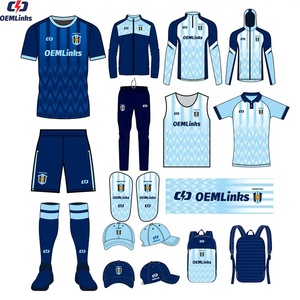
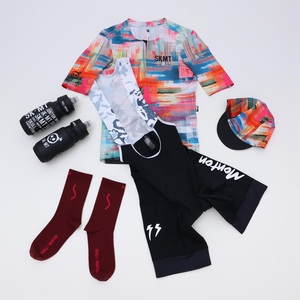
Operating as a fully integrated contract manufacturing powerhouse, our manufacturing framework unites automated textile knitting, computerized pattern cutting, Italian sublimation dye systems, and certified four-tier quality control under one roof.
Unlike trading intermediaries, we control raw yarn procurement, knitting, sublimation printing, embroidery, tackle twill, cut-and-sew assembly, and final iron-packing in-house. This centralized control virtually eliminates handoff delays and defect leakage.
All functional basketball fabrics and water-based sublimation inks meet strict international non-toxicity standards. Our production processes adhere strictly to ISO 9001:2015 quality control parameters, offering complete lot traceability for global compliance.
Rapid proto-sampling completed in 7 to 10 days from confirmed digital vector tech packs. Standard full-scale bulk container shipments dispatch within 30 to 45 days, supported by direct customs clearance coordination across FOB, CIF, and DDP terms.
Basketball team uniforms endure some of the highest dynamic friction coefficients, rapid burst acceleration, and continuous moisture perspiration cycles in modern competitive athletics. A generic polyester mesh fails within multiple tournament washes through seam failure or yarn abrasion. As a Tier-1 China sports apparel manufacturer, we engineer specialized fabric matrices engineered around three primary technical pillars:
1. Dual-Sided Hydrophobic Micro-Mesh (160–180 GSM): Utilizing a modified honeycomb knitting formation, the inner surface absorbs sweat instantly from the player’s epidermis via capillary action, pulling it through micro-perforated capillary tubes to the outer surface where ambient air current facilitates rapid flash evaporation.
2. High-Burst Multi-Filament Interlock: For collegiate and professional match kits, we utilize a dense 200–220 GSM high-gauge filament interlock polyester featuring 8–10% elastane content. This structure resists baseline grappling, shirt-pulling, and floor slide abrasion while offering zero transparency under intense arena floodlights.
3. Anti-Bacterial & Odor-Neutralizing Finishes: Integrated silver-ion (Ag+) antimicrobial baths applied during the fabric finishing phase disrupt bacterial lipid membranes, permanently neutralizing sweat-induced odor molecules and ensuring garments survive demanding season schedules without degradation.
| Performance Parameter | Pro-League Standard | Collegiate / High School Club | Recreational / Promotional |
|---|---|---|---|
| Primary Fabric Composition | 100% Recycled Polyester (rPET) Interlock + Spandex lateral inserts | 100% Filament Dri-Wick Birdseye Micro-Mesh | Open-Hole Polyester Poly-Mesh + Poly Lining |
| Fabric Weight (GSM) | 190 – 210 GSM (Burst-Resistant) | 160 – 180 GSM (Balanced Cooling) | 140 – 150 GSM (Cost Optimized) |
| Color Fastness (AATCC 61) | Grade 4.5+ (High-Temp Commercial Wash) | Grade 4.0 (Standard Wash Cycles) | Grade 3.5 – 4.0 |
| Lettering & Numbering | Laser-Cut Multi-Layer Tackle Twill / High-Density Silicone 3D | Full Digital Thermal Dye Sublimation | Plastisol Screen Print / Thermal Vinyl Heat Press |
| Seam Construction | 4-Needle 6-Thread Flatlock + Reinforced Armhole Overlock | Double-Needle Flat Seam with Bartack Stress Points | Standard 3-Thread Industrial Overlock |
| Inspection Standard | AQL 1.5 Strict Industrial Visual & Pull-Tolerance | AQL 2.5 Major / 4.0 Minor Global Export | AQL 4.0 Standard Batch Inspection |
B2B sportswear procurement is transitioning rapidly from basic mass-production sourcing toward high-tech customization, environmental sustainability metrics, and rapid-response modular supply chains. Forward-thinking procurement teams must factor the following macro-developments into their multi-year vendor strategy.
By 2026, over 65% of premier professional sports organizations and university leagues mandate certified post-consumer recycled fabrics (GRS - Global Recycled Standard). Our factory leads this shift by substituting virgin polyester filaments with certified ocean-bound and recycled PET flake polymers without compromising tensile tear strength or print brilliance.
Gone are the eras where distributors tied capital in massive off-season warehouse bulk inventories. The modern standard demands automated print-on-demand replenishment. Using high-speed industrial dye-sublimation plotters running waterless sublimation inks, we allow partner brands to submit dynamic mid-season reorders with MOQs as low as 20 units per squad without tooling surcharges.
Laser-cut targeted thermal mapping is revolutionizing jersey design. Using digital body-temperature heat maps of professional basketball players during game action, our computerized laser cutters integrate specialized micro-venting clusters along the lower lumbar region, mid-spine, and lateral rib corridors to maximize airflow without weakening garment structural integrity.
While basic apparel production continues migrating toward lower-cost Southeast Asian destinations, high-performance athletic teamwear—particularly sublimated basketball uniforms—remains heavily anchored in China's advanced textile industrial clusters (notably Guangdong, Zhejiang, and Fujian). The underlying competitive advantages are clear:
Unrivaled Chemical & Dyestuff Supply Chains: China produces the world’s most stable, disperse-dye thermal sublimation chemicals and Italian-engineered digital sublimation inks. In sublimated teamwear, inferior dye chemistry causes "cracking" under stretch and color degradation when exposed to intense UV gym lighting or high-temperature commercial dryers. China's chemical infrastructure delivers Delta E color consistency under 0.8 across repeat production batches years apart.
Automated CNC Cutting & Seam Precision: Producing complex basketball uniforms involving side-panel color matching, sublimated gradient continuity, and precise number placement requires digital optical CNC fabric cutters. Our factory utilizes high-precision optical laser beds that automatically recognize sublimation print registration marks on the knitted rolls, cutting panels with sub-millimeter precision before human hands touch the garment at the sewing stations.
Every order flows through a calibrated, audit-ready 6-stage milestone protocol. Sourcing directors receive direct digital visual verification at every critical production tollgate to eliminate surprises.
Comprehensive design evaluation reviewing artwork vectors (AI/PDF), PMS Pantone spot colors, grade size ratios, tackle twill embroidery digitizing, and seam construction specs. Our engineering team catches potential distortion points before sampling.
We generate digital color mini-swatches and strike-off prints onto the exact production-grade polyester fabric. Strike-offs are assessed under standard D65 lightbox conditions to verify absolute Pantone hue alignment.
Creation of a full physical proto-set (jersey and matching game shorts) within 7–10 days. The prototype is stress-tested for seam stretch recovery, neckband elasticity, and accurate proportional drape across player dimensions.
Following formal buyer approval, raw performance rolls undergo computer-guided automated spreading and laser cutting. Sublimation paper transfer occurs via calibrated continuous rotary drums running at 210°C under precise pneumatic pressure.
Garments pass through multi-station assembly cells: shoulder bonding, collar setting, armhole binding, flatlock seam finishing, and tackle twill application. Every single piece is hand-measured against graded specification sheets.
Retail-ready finishing including custom printed woven neck tags, hang tags with barcode stickers, desiccant pouches, and master carton palletization. Complete customs export paperwork generated for air freight or maritime containers.
Essential guidance covering technical requirements, minimum volume thresholds, international export logistics, and private-label customization options.
Partner directly with China's premier basketball team uniform and performance athletic apparel manufacturing facility. Access factory-direct wholesale pricing, rapid prototype development, and reliable international delivery for your forthcoming season collection.