Engineered for marathoners, track athletes, and cross-training regimes. Each unit leverages moisture-wicking microfilaments, mechanical four-way stretch, and bonded ergonomic seams tested across high friction zones.
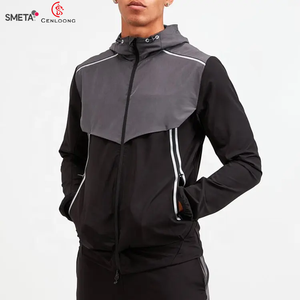
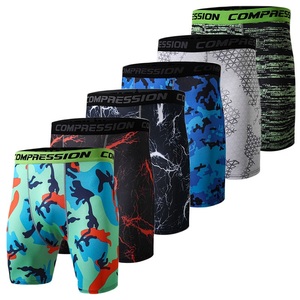
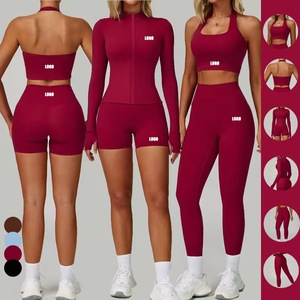
Evaluating tier-1 athletic apparel contract manufacturing clusters based on functional textile knitting, bonded seam precision, lead-time elasticity, and compliance standards.
| Manufacturing Cluster & Region | Primary Technical Specialization | Average Lead Time (Proto / Bulk) | Core Compliance Certifications | Strategic Tier Rating |
|---|---|---|---|---|
| Verena Sport (Sialkot, Pakistan) | Sublimated technical running singlets, welded outer windbreakers, circular knit compression tights | 7-10 Days / 30-45 Days | ISO 9001, OEKO-TEX Standard 100, BSCI Audit Ready | Tier 1 Direct OEM |
| Binh Duong Textile Corridor (Vietnam) | Large-scale polyester microfiber bonding, bonded hyper-light marathons jackets | 14-21 Days / 60-90 Days | WRAP, Higg Index, bluesign® | Tier 1 Enterprise |
| Taoyuan Functional Textile Cluster (Taiwan) | Advanced bio-nylon yarn extrusion, phase-change cooling fabrics, reflective treatments | 15-25 Days / 70-85 Days | GRS Certified, bluesign®, Oeko-Tex Class I | Raw Material & OEM |
| Porto Athletic Manufacturing District (Portugal) | Seamless circular-knit running base layers, ultrafine Merino wool hybrid apparel | 10-14 Days / 45-60 Days | GOTS, SMETA, ISO 14001 | European Nearshore |
| Fujian Coastal Manufacturing Hub (China) | Ultra-sonic welded rainwear, mechanical stretch woven track shells, automated laser cutting | 10-15 Days / 45-60 Days | ISO 9001, SA8000, GRS | High-Volume Specialist |
| Izmir Performance Knit Cluster (Turkey) | Recycled polyester running t-shirts, modal activewear blends, low-transit EU replenishment | 12-18 Days / 40-50 Days | Sedex, OEKO-TEX Step, GRS | Nearshore Fast-Turn |
How progressive running labels are transforming high-mileage garment performance through advanced polymer chemistry, aerodynamic patterning, and sensory thermo-regulation.
Moving beyond basic topical wicking finishes, next-gen running knits utilize bi-component differential structures. Hydrophobic continuous filaments on the interior skin interface push perspiration outward toward hydrophilic outer micro-channels, maintaining dry-surface skin contact even during multi-hour endurance efforts.
Body-mapping thermo-graphic analyses guide automated laser cutters to micro-perforate high-perspiration quadrants (spine channels, underarms, sternum). Simultaneously, multi-needle flatlock seam configurations and bonded thermo-polyurethane (TPU) hem tapes eliminate mechanical friction across friction-critical areas.
Rather than relying on chemical wash finishes that degrade after 20 commercial laundry cycles, modern running fibers incorporate nano-sized crushed jade or ceramic minerals directly into the polymer dope during extrusion. This creates permanent conductive cooling properties, reducing core skin temperature by 1.2°C to 1.8°C.
Engineered graduated elastomeric arrays provide targeted kinetic support to hamstring and quadricep muscle bellies. Controlled variable elasticity dampens muscle oscillatory vibrations on downhill impacts, diminishing muscular fatigue indices and accelerating lactic acid clearance post-effort.
Environmental compliance mandates a total shift away from long-chain fluorinated hydrocarbons (C8/C6). Modern technical windbreakers and shell jackets utilize non-fluorinated, plant-based silicones or dendrimer chemistry, achieving ISO 4920 spray ratings of 90+ while preserving microporous air permeability.
Visibility engineering now demands seamless night-running protection. Factories leverage high-frequency heat-transfer reflective films featuring microscopic hemispherical glass beads that return light beams directly to vehicle headlamps from distances exceeding 160 meters without sacrificing base-fabric elongation.
Structural shifts in global sourcing require brand directors to rethink minimum order quantities, trade lane resilience, and end-to-end material traceability.
Over-reliance on East Asian single-country manufacturing has given way to multi-node geographic hedging. Pakistan’s world-renowned textile cluster in Sialkot provides an optimal balance: duty access, generational sewing dexterity, vertically integrated knitting, and direct factory pricing devoid of export broker markups.
To safeguard working capital, modern activewear labels have abandoned monolithic 10,000-unit commitments per style/colorway. Tier-1 suppliers now offer modular batch runs (100–300 pcs) supported by digital sublimation print bars, rapid automated cutting tables, and rolling replenishment workflows.
Forthcoming EU eco-design directives require verifiable transparency across the garment lifecycle. Procurement contracts increasingly specify recycled post-consumer PET (rPET), bio-mass polyamides, and QR-encoded data passports documenting chemical safety, factory carbon footprints, and fiber mono-materiality for post-use recycling.
Operating from the heart of Sialkot since 2005, Verena Sport combines deep sports apparel craft with certified industrial governance, serving premier retail brands and sporting clubs in over 50 nations.
Pattern engineering, grading, computer-aided marker cutting, computerized flatlock stitching, full-color sublimation, screen-printing, embroidery, and inline needle-detection occur in one owned facility. Removing third-party contractors prevents hand-off errors, shade mismatches, and scheduling friction.
We transform rough design briefs or 2D tech packs into market-ready retail products. Sourcing custom yarn blends, developing custom Pantone dyes, applying branded heat-transfer labels, woven neck tags, hang tags, and custom retail packaging are completely handled under client branding.
Fit and aesthetic proto samples are produced and dispatched within 7–10 working days. Standard bulk production windows range between 30 and 45 calendar days post-approval. Merchandisers provide photographic milestones at fabric arrival, inline sewing, and packing.
Every batch of functional fabric conforms to strict AATCC and ISO dimensional stability standards, with colorfastness ratings exceeding 4.0 after dry rubbing and laundering. Full compliance documentation and factory audit files are made available upon buyer request.
With twenty years of active export operations to the United States, United Kingdom, European Union, Australia, and Canada, our export desk handles bonded freight, bill of lading documentation, export declarations, and certificate of origin paperwork without unexpected buyer surprises.
Eliminate misunderstandings caused by third-party trading entities. Our export merchandising managers possess deep technical pattern literacy and functional textile expertise, communicating directly via email, video conference, and instant messaging channels with 24-hour turnaround commitments.
Clear answers to commercial and technical questions commonly addressed when evaluating new running apparel and sportswear suppliers.
We review your tech pack, CAD drawings, or physical reference garments and match appropriate yarn weight, knit construction, and trims. Initial proto and fit samples are completed within 7 to 10 working days, shipped directly via express courier with comprehensive spec verification sheets.
We employ 4-needle 6-thread flatlock machines equipped with differential feed settings to prevent wavy seams on elastic poly-spandex blends. Thread tension is calibrated precisely for high-stretch movements, and critical chafing zones are tape-bonded with heat-activated TPU adhesives.
Our MOQs adapt to specific fabric categories and customization complexity. Standard runs start from 50 to 100 units per colorway for customized sublimation teamwear, while specialized custom-milled functional knits or outerwear shells generally begin at 250 to 500 units per style, allowing brands to launch multi-size collections efficiently.
Our manufacturing management follows ISO 9001 certified Quality Management Systems. Our performance fabric mills provide OEKO-TEX Standard 100 Class II compliance ensuring zero harmful carcinogens, formaldehydes, or banned phthalates, supporting hassle-free clearance into EU, UK, and North American consumer markets.
We use high-grade disperse inks paired with calibrated high-pressure thermal transfer calenders operating at 205°C. This guarantees optimal dye penetration deep into the polyester core, yielding colorfastness to washing and perspiration ratings of 4.5+ under ISO 105-C06 testing protocols.
We regularly ship on FOB (Free On Board) Karachi or Lahore sea/air terminals, and CIF (Cost, Insurance, and Freight) to major destination ports across Europe, North America, Oceania, and the GCC. Air courier consolidation is available for urgent seasonal collections and capsule launches.
Whether you require full-package OEM production from your original tech pack, or wish to sample from our existing high-performance running catalog, our merchandising team provides prompt technical audits and pricing within 24 hours.
