Explore high-resilience, multi-filament football kits manufactured with disperse Italian reactive dyes, dynamic ergonomics, and athletic contouring for global sports brands, franchises, and tournament events.
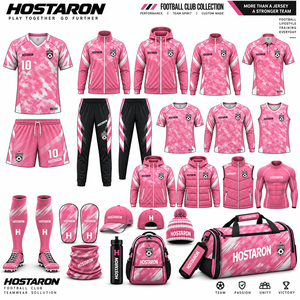
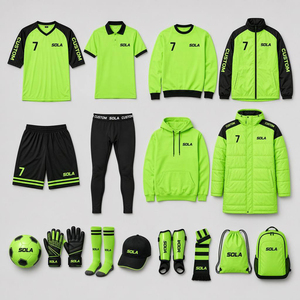
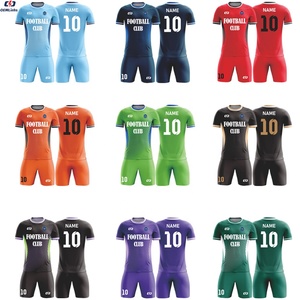
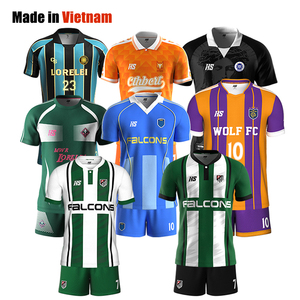
In modern performance sportswear manufacturing, dye-sublimation printing represents an evolutionary shift away from legacy screen printing and heavy plasticized vinyl transfers. For institutional athletic clubs, academic sports organizations, and international retail brand distributors, sublimation permanently fuses gaseous disperse inks directly into the polymer matrix of virgin or recycled polyester (rPET) fibers at temperatures exceeding 200°C. This chemical bonding ensures that complex multi-color crests, typography, hyper-detailed geometric gradients, and corporate sponsor branding exhibit zero hand-feel (zero hand touch), retain 100% fabric pore breathability, and are unconditionally immune to peeling, bubbling, cracking, or color fading across industrial wash cycles.
As international supply chain executives adapt to shorter product lifecycles, our fully integrated Sialkot manufacturing complex eliminates tiered middleman costs. We balance structural integrity with mechanical moisture management—combining hydro-conductive polyester micro-yarns with precision flatlock dynamic seaming. Understanding the shifting market dynamics of the activewear space is essential for inventory agility and margin control.
A systematic analysis of technical, environmental, and inventory management developments governing commercial football uniform production through 2026 and beyond.
Global apparel directives and corporate environmental compliance (ESG) are driving high volume procurement away from virgin synthetics. The modern global standard is GRS (Global Recycled Standard) certified rPET derived from post-consumer polyethylene terephthalate bottles.
Single-fabric construction is obsolete at professional athletic tiers. Progressive soccer kits merge multiple synthetic fabric weights into zoned athletic heat-dispersion garments that respond to player physiological stress.
Inventory depreciation risk has incentivized distributors to move away from deep static warehouse volumes. Digital industrial printing setups allow rapid-batch production runs without costly tooling setups.
Comprehensive engineering matrices detailing fabric density, stitch tension, colorfastness standards, and OEM options available for private label programs.
| Performance Parameter | Commercial Grade Standard | Verena Sport OEM Factory Baseline | Operational Benefit |
|---|---|---|---|
| Fabric Composition | 100% Virgin Polyester (Standard) | 100% Micro-Filament Interlock / rPET Recycled Poly / Spandex blends | Silky skin-feel, superior hydrophobic moisture ejection, zero chafing |
| Grammage (GSM) | 130 - 180 GSM Single Weight | Dual-zone: 155 GSM Body / 125 GSM Back-Vent Diamond Mesh | Optimal balance between anti-abrasion durability and dynamic weight reduction |
| Dye Fastness (ISO 105-C06) | Grade 3-4 (Moderate Wash Degradation) | Grade 4.5+ Disperse Italian Inks (Zero bleed under 60°C laundering) | Indefinite color saturation, vibrant neon fidelity, zero bleed into light contrasts |
| Stitch Density & Type | 3-thread overlock (10-12 stitches/inch) | 4-thread safety interlock + 6-thread active flatlock (14-16 SPI) | Tear-proof seam resilience against dynamic tackles and mechanical pulling |
| Branding Application | Basic Heat Transfers / Rubber Badges | Full Ink Impregnation, 3D Silicone Transfer, Woven Appliqué, Ultrasonic Patches | Versatile brand positioning, professional club aesthetics, friction reduction |
Why Tier-1 international sporting brands, regional distributors, and tournament leagues establish long-term sourcing contracts with Verena Sport in Sialkot, Pakistan.
Unlike trading brokerages or assembly shops, our comprehensive production infrastructure consolidates automated CAD pattern grading, precision laser fabric cutting, large-format rotary heat sublimation, multi-head computer embroidery, and ISO-monitored stitching under one facility in Sialkot, Pakistan.
Our operations function under strictly verified ISO 9001 Quality Management standards. Fabrics adhere to OEKO-TEX Standard 100 Class I chemical safety thresholds, ensuring all manufactured athletic garments are hypoallergenic, phthalate-free, non-toxic, and legal for unrestricted sale across North American and European borders.
Backed by over twenty years of active export presence, we streamline maritime freight, intermodal haulage, and air courier dispatching under transparent Incoterms (FOB Karachi, CIF, and DDP to major distribution centers in the United States, United Kingdom, European Union, Australia, and the Middle East).
Direct technical and operational clarifications answering critical queries raised by sportswear product managers, buying houses, and corporate apparel procurement officers.
Consult with our in-house technical merchandising engineers, request comprehensive physical fabric swatches, or configure an OEM football line calibrated to your exact retail specifications.
Get Catalog