Explore precision-manufactured OEM/ODM apparel manufactured under ISO 9001 quality systems with full digital sublimation and private label customization.
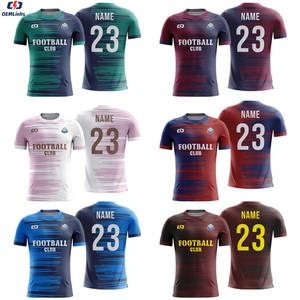
The contemporary performance teamwear landscape demands extreme durability, hyper-wicking thermoregulation, and non-restrictive ergonomic mobility.
Modern soccer jerseys utilize engineered micro-polyester interlock knits featuring channeled denier cross-sections. This architecture exploits hydrodynamic pressure differentials, pulling perspiration away from the athlete's dermis toward the garment exterior for instant evaporative dispersion.
By mapping human thermodynamic exertion zones during high-intensity 90-minute matches, our automated circular knitting machinery creates jacquard pinpoint mesh structures under the arms, chest, and lumbar zones without requiring structurally weak secondary cut-and-sew panels.
Our industrial sublimation units apply Italian disperse dyes at 210°C under precise 6-bar mechanical roller tension. The dye molecules transition instantly from solid to gas, bonding molecularly with synthetic polyester chains to ensure 0% fading, zero hand-feel stiffness, and absolute breathability.
| Performance Dimension | OEM Standard Configuration | ODM Elite Match Specification | Testing & Compliance Protocol |
|---|---|---|---|
| Fabric Density (Weight) | 140 - 155 GSM Birdseye Interlock | 160 - 180 GSM Micro-Ribbed Spandex Poly | ASTM D3776 Standard Test Method |
| Color Fastness (Perspiration) | Grade 4.0 Minimum | Grade 4.5+ (Spectrophotometer verified) | ISO 105-E04 / AATCC 15 |
| Tensile & Seam Bursting Strength | ≥ 220 kPa Multi-thread Overlock | ≥ 350 kPa Reinforced Flatlock + Bartack | ASTM D3786 Diaphragm Bursting |
| Sublimation Ink Chemistry | Eco-Solvent Disperse Formulations | Water-Based OEKO-TEX Standard 100 | Zero Azo-Dyes / REACH Compliant |
| Crest & Numbering Options | Silkscreen / PU Vinyl Heat Transfer | 3D High-Density Molded TPU / Silicone Badges | 50+ Commercial Wash Cycles @ 40°C |
Strategic analysis for brand directors, club procurement managers, and sportswear buyers navigating shifting international trade landscapes, circular compliance, and agile manufacturing.
Global regulatory pressure, led by EU Corporate Sustainability Due Diligence rules, is pushing professional football clubs and regional leagues toward certified post-consumer recycled yarns (rPET). These virgin-equivalent fibers lower carbon footprints by 65% while retaining identical tensile strength and hydrophilic capillary dispersion.
Aerodynamic surface texturing is transitioning from elite wind tunnel cycling kits into football jerseys. Micro-embossed chevron texturing on forearm sleeves and dynamic ribbing reduce drag and optimize fluid boundary layers during high-speed sprints, representing a high-margin value-add for ODM product developers.
Wholesale distribution is abandoning rigid 12-month advance buying cycles. Forward-thinking brands now leverage modular OEM suppliers capable of executing 100-to-500-unit rapid turnaround reorders within 12 business days, drastically mitigating stockout penalties while eliminating terminal deadstock liabilities.
Non-migrating silver ion and bio-based zinc pyrithione finishes permanently bonded within yarn interstices prevent bacterial growth and sweat degradation. This technology maintains garment freshness through grueling multi-day tournaments and continuous training sessions without washing out.
Sialkot stands as the undisputed global capital for hand-stitched and thermally bonded athletic gear, handling international tournament contracts with unmatched supply chain depth and cost efficiency.
Unlike trading intermediaries that subcontract production across fragmented workshops, our facility consolidates computer-aided pattern digitization, laser cloth cutting, automated dye-sublimation calendering, dedicated sewing lines, and automated packaging under one unified management system. This ensures uninterrupted batch-to-batch color match, seam integrity, and guaranteed ship windows.
We convert rough design concepts or detailed Adobe Illustrator tech packs into export-grade collections. Our development suite delivers custom woven high-definition neck labels, laser-etched silicone badges, custom-branded hang tags, branded biodegradable polybags, and retail-ready carton packing optimized for international container shipping.
Full engineering evaluation of grading rules, seam tensions, fabric weights, and print tolerances before cutting.
Digital sublimation paper proofs and spectrophotometer-calibrated swatches dispatched via express air courier.
Finished pre-production sample delivered within 7 to 10 days for tactile fit, drape, and stitch inspection.
Rigorous inline quality gates checking seam tensile integrity, tension puckering, and graphic alignment.
Comprehensive pre-shipment audit covering dimensions, barcoding, packaging purity, and carton drop integrity.
Complete export documentation, customs clearance, and global air/sea forwarding to over 50 global destinations.
Authoritative technical, commercial, and logistical clarifications for global sourcing directors and supply chain managers.
Our standard production MOQ for fully custom sublimated soccer jerseys is structured at 50 units per design, accommodating mixed sizes (e.g., Youth S through Adult 3XL). For specialized stock fabrics or pre-dyed cut-and-sew collections requiring custom pantone dyeing, MOQs generally start at 200 units per colorway. We also offer dedicated sample production runs (1 to 5 units) prior to bulk commercial authorization.
Color matching is controlled through digital RIP profiling and X-Rite spectrophotometer calibration against physical Pantone Formula Guides (TPG/TCX/PMS). We maintain secure digital production profiles for every customer order. When reorders are placed, identical dispersed dye curves, sublimation dwell temperatures, and calendering roll speeds are applied, guaranteeing a Delta-E (ΔE) color variance threshold of less than 1.0.
We provide all primary modern teamwear cresting and decoration methods: edge-to-edge all-over disperse dye-sublimation; high-density 3D molded heat-seal silicone emblems; sonic-welded TPU crests; traditional laser-cut twill with dense satin embroidery borders; screen-printed silicone grippers; and reflective high-visibility polyurethane heat-transfers engineered for 50+ commercial wash cycles.
Prototyping and pre-production fit samples are ready in 7 to 10 working days. Upon final written sample sign-off and lab-dip approval, bulk commercial cutting and sewing takes approximately 25 to 35 business days for quantities up to 5,000 units. For urgent institutional and tournament replenishment, expedited 14-day production slots can be arranged via priority lines.
Our manufacturing operations are ISO 9001:2015 certified for Quality Management Systems. We exclusively utilize raw synthetic polyester fabrics and elastane blends certified under OEKO-TEX Standard 100 (Class I and II), certifying complete absence of harmful azo dyes, formaldehyde, phthalates, or heavy metals. Full audit documentation, child-labor-free certifications, and social compliance reports are available upon request.
We regularly export under FOB (Karachi Port / Sialkot International Airport), CIF, CFR, and DDP (Delivered Duty Paid) terms depending on buyer preference. We partner with tier-1 international freight forwarders including DHL, FedEx Express, Maersk, and MSC, handling all export documentation, Certificates of Origin, commercial invoices, and tariff classification to streamline customs clearance in the USA, UK, EU, Canada, and Australia.
Access our comprehensive export catalog, physical fabric swatch portfolios, technical sizing specifications, and volume pricing matrices for club, brand, and retail distribution.