Bridging polymer fabric science with artisanal pattern tailoring. Verena Sport provides turn-key OEM and ODM manufacturing capabilities for independent athleisure disruptors and scaled global fitness brands seeking rigorous production governance in Sialkot, Pakistan.
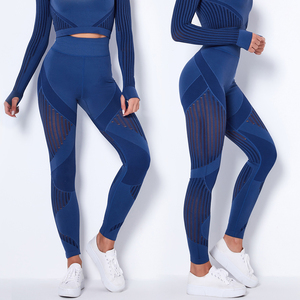
The transition of yoga leggings from niche fitness accessories to ubiquitous lifestyle garments demands unprecedented rigor from modern original equipment manufacturers (OEMs). Today's athleisure consumer expects a confluence of zero-sheer opacity ("squat-proof integrity"), featherlight second-skin touch, ergonomic structural contouring, and sustained elasticity throughout prolonged wash-and-wear cycles. For procurement specialists, product developers, and private label merchandisers, partner selection must pivot on scientific yarn composition, precision knitting machinery, and end-to-end quality assurance mechanisms.
At Verena Sport, our industrial plant in Sialkot, Pakistan, combines twenty years of specialized textile craft with state-of-the-art circular knitting arrays and automated cut-and-sew operations. Producing high-performance activewear requires an intimate comprehension of yarn tensioning, elastane degrade profiles, stitch mechanics, and the dynamic physiology of the human muscular system under physical exertion.
We leverage specialized micro-filament Nylon 6.6 combined with virgin DuPont Lycra or eco-recycled Creora® elastane. This creates micro-channels that optimize evaporative cooling while preventing yarn slippage under deep biomechanical flexion.
Assembling activewear demands high-yield 4-needle 6-thread flatlock machines using micro-textured polyester thread. This achieves zero-friction seam low-profiling that prevents chafing and preserves over 95% base fabric stretch recovery.
Standard retail failures stem from single-jersey coarse knitting. We utilize ultra-fine 28-gauge to 32-gauge high-density interlock machines, ensuring absolute zero grin-through under 120% horizontal and vertical elongation stretch tests.
Procuring custom yoga apparel requires explicit production standards. Below is our baseline technical specification sheet for global OEM brand programs:
| Engineering Attribute | Verena Sport OEM Standard | Testing Protocol / Industry Benchmark |
|---|---|---|
| Fabric Blends Available | Nylon 6.6/Spandex, Recycled Polyester (rPET), Bamboo Viscose, Organic Cotton Interlock | OEKO-TEX Standard 100 Class 1, GRS 4.0 Certified |
| Areal Fabric Density (GSM) | 200 GSM (Ultra-light aerated) to 320 GSM (High-compression shapewear) | ASTM D3776 Standard Test Methods for Mass Per Unit Area |
| Color Fastness Performance | Grade 4.5+ against laundering, acidic perspiration, and friction/rubbing | ISO 105-C06 / AATCC 61 Accelerated Laundering |
| Four-Way Stretch Ratio | 120%–140% Weft; 90%–110% Warp with ≥96% immediate modulus rebound | ASTM D2594 Elastic Fabric Dynamic Recovery Test |
| Stitching Tensile Integrity | 4-Needle 6-Thread ISO 607 Flatlock Seam Assemblies (≥16 stitches per inch) | ASTM D1683 Seam Failure in Woven and Knitted Apparel |
| Branding Decor Options | Silicone matte heat transfer, Sublimation edge-print, Jacquard bands, Reflective 3M | AATCC 88B Wash Durability (≥50 Commercial Cycles) |
The global athletic apparel industry is transforming rapidly. Merchandisers who anticipate shifting retail demands will outperform those relying on outdated cut-and-sew conventions. Through our supply partnerships across Europe, North America, and Australia, we identify four macro trends steering activewear sourcing through the next five years:
1. Decarbonized and Recycled Technical Polymers: Traditional virgin petroleum synthetics are facing aggressive regulatory and consumer pushback. Top-tier brands are switching to post-consumer Ocean Waste Polyamide (rNylon) and closed-loop Recycled Polyethylene (rPET). These materials maintain identical shear-modulus performance to virgin fibers while dropping supply chain carbon footprints by 45%.
2. Posture Feedback & Ergonomic Architecture: The crossover between physical therapy and fitness clothing is driving demand for multi-density mapped paneling. Instead of single-compression leggings, modern designs employ differentiated tension bands across the hamstrings, gluteus medius, and lower lumbar. This supports posture during high-intensity training and studio classes.
3. Anti-Microbial Hydrophilic Fiber Modifications: Consumers are rejecting chemical topical washes that wash out after ten cycles. Sourcing teams are turning to yarn-level innovations, such as zinc-oxide infusions and permanent silver-ion extrusions. These provide lifetime bacteriostatic odor control and superior moisture transport.
4. Inclusive Anatomical Tailoring: Standard automated pattern sizing often fails when extended to extended sizes, causing uneven waistband sagging and knee pouching. High-retention activewear requires independent 3D virtual avatar simulation and customized grade scales to maintain compression curves consistently from XS through 6XL.
Founded in 2005 in Sialkot, Pakistan, Verena Sport delivers the manufacturing precision, technical capacity, and social compliance demanded by world-class activewear retailers.
Cutting, printing, embroidery, stitching, and pressing occur under one roof in Sialkot. No decentralized sub-contracting risk ensures dependable lead times and consistent product sizing.
Certified inline inspection protocols using AQL 2.5 standards. Fabric lab dip analysis, wash audits, and chemical compliance documents are accessible for third-party auditing.
Move swiftly from tech pack to production-ready sample. Our in-house pattern-makers optimize seam lines, waistband curvature, and gusset positions within days.
Beyond cut-and-sew, we offer complete private-label support: woven damask branding, laser-etched drawstrings, thermo-transfer wash icons, and retail polybags.
We export to over 50 countries, including the USA, UK, Germany, and Australia. We offer FOB, CIF, or DDP terms with all customs paperwork handled seamlessly.
Work directly with English-speaking textile engineers and production managers. Receive regular photo and video milestones without trading company markups.
Key technical, commercial, and operational considerations when launching OEM yoga apparel manufacturing lines.
Our baseline MOQ is tiered according to fabric selection. For stock catalog performance poly-spandex blends, MOQs start as low as 100 to 150 pieces per style/colorway across flexible size distributions. For bespoke yarn-dyed, custom pantone-milled circular fabrics, MOQs typically begin around 300 to 500 units to satisfy mill-level knitting economics.
We guarantee 100% squat-proof opacity by employing dual-knit high-density interlock machines (minimum 28-gauge) combined with a high-spandex balance (typically 20% to 27%). Every fabric roll goes through horizontal-pull spectrophotometer lightbox testing before it enters automated precision cutting tables.
Yes. If you provide a physical benchmark garment or fabric swatch, our laboratory analyzes the fiber cross-section, weight (GSM), brushing technique, and tensile recovery profile. We can systematically match buttery-soft peach finishes, slick compressive wraps, or ribbed structural tactile knits.
Prototyping, fit samples, and swatch lab dips generally require 7 to 10 working days. Once client approvals, physical sign-offs, and tech pack confirmations are complete, full bulk production is delivered within 30 to 45 business days, depending on styling complexity and trim logistics.
We utilize precision 4-needle 6-thread flatlock stitching (ISO 607) for main inseams and front rises to keep interior seams completely flush against the skin. For high-tension junctions, we integrate bar-tacking, ergonomic triangular or diamond gusset insets, and bonded clean-edge waistbands.
As an experienced contract manufacturer since 2005, Verena Sport operates under comprehensive Non-Disclosure Agreements (NDAs). Your proprietary patterns, tech-pack metrics, custom graphic files, and custom branded packaging are securely archived and never shared with other clients or third parties.
Consult with our technical activewear merchandising engineers. Review physical fabric swatches, explore sustainable yarn developments, and launch production with confidence.
