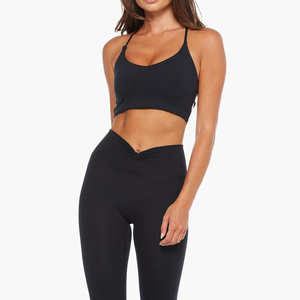
Explore 8 precision-engineered performance apparel lines manufactured directly within our ISO 9001-certified Sialkot production cluster. Fully configurable for custom GSM, technical yarn compositions, sublimated graphics, and custom branding.
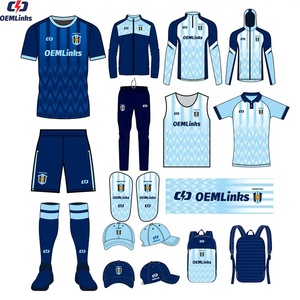
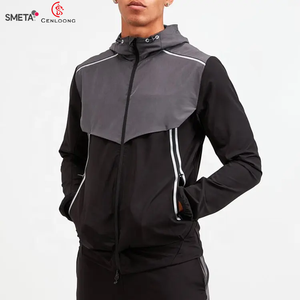
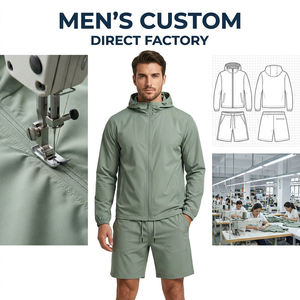
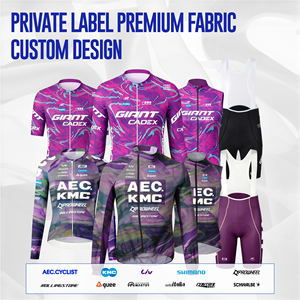
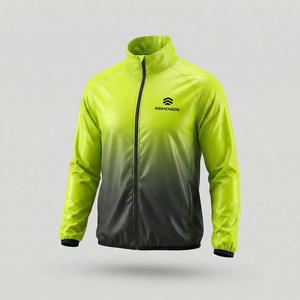
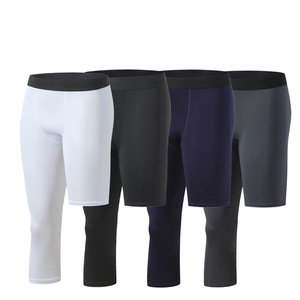
Eliminating third-party trading intermediaries through vertically integrated garment mills in Sialkot, Pakistan. From yarn inspection to ultrasonic seam bonding and final retail export packaging.
Pattern CAD grading, digital sublimation printing, laser cutting, 4-needle 6-thread flatlock stitching, and final quality gates occur entirely within our owned production facilities. By centralizing operations under one roof, we eliminate subcontractor lead-time drift and ensure rigid lot-to-lot consistency.
We source certified eco-compliant yarns tested strictly for banned substances, azo dyes, and skin sensitizers. Operating under ISO 9001:2015 Quality Management protocols, our manufacturing floor maintains clean-room standard fabric inspection, inline needle detectors, and calibrated bursting-strength tension meters.
In the fast-moving athleisure landscape, speed-to-market defines profitability. Our dedicated sampling workshop outputs counter-samples within 7 to 10 working days directly from your digital tech pack. Scaled bulk orders dispatch systematically within 30 to 45 days backed by proactive daily milestone tracking.
Transforming wholesale concepts into standalone boutique lines. We provide comprehensive branding ecosystems including ultrasonic high-density heat transfers, silicone raised micro-injections, jacquard waistband weaving, OEKO-TEX woven damask tags, custom barcode labeling, and biodegradable zipper frosted bags.
With more than 20 years supplying athletic apparel across 50+ countries including the United States, United Kingdom, Germany, France, Canada, and Australia, our compliance division guarantees seamless international commercial customs clearance, certificate of origin validation, and streamlined air/sea freight routing.
Work directly with English-speaking textile engineers and pattern masters rather than commission-based sales representatives. Enjoy clear technical consultations regarding yarn blends, seam elongation specs, shrinkage stabilization, and precise pantone color matches with transparent live video conferencing.
An analytical blueprint on technical yarn innovation, circular supply chain mandates, smart compression ergonomics, and near-mill cluster resilience for procurement directors.
The global athleisure sector has decisively outgrown its origins as a casual derivative of athletic wear. Today, it constitutes an independent, multi-billion-dollar discipline bridging high-performance alpine gear engineering with everyday executive and leisure aesthetics. For brand procurement officers, sourcing managers, and private label apparel founders, navigating this landscape requires moving beyond generic cut-and-sew relationships into deeply strategic manufacturing partnerships characterized by fabric science, lifecycle accountability, and digital workflow synchronization.
The contemporary performance consumer demands garments with zero compromise: extreme four-way stretch, matte squat-proof opacity, tactile peach-skin softness, and bio-based environmental compliance. Factory partners lacking in-house lab-testing and computerized pattern-grading cannot sustain the sub-2% variance thresholds required by modern direct-to-consumer athletic brands.
Strategic purchasing teams are actively restructuring their vendor matrices to adapt to several irreversible market vectors. The most prominent shifts driving RFP and purchasing decisions over the next five years include:
A. Decarbonized Circularity and Traceable Feedstocks: Conventional virgin petroleum-derived polyester and nylon are facing intensifying regulatory scrutiny across the EU and North American markets. Procurement leaders are prioritizing OEM suppliers offering certified recycled polyamides (such as ocean-bound recycled nylon), bio-polymer elastanes, and solvent-free waterborne polyurethanes for technical outerwear. Traceability from raw flake to finished yardage through verified Scope 1–3 documentation is swiftly becoming an invoice prerequisite.
B. Near-Mill Manufacturing Hubs and Cluster Synergy: The disruption of isolated supply chains has accelerated the demand for concentrated manufacturing clusters. Sialkot, Pakistan, represents a historically unique global hub where spinning, circular knitting, sublimation dyeworks, embroidery, precision cutting, and international logistics converge within a tight 25-kilometer radius. This close geographic proximity compresses carbon footprints, shortens yarn-to-dock transit, and insulates international buyers from complex multi-country customs bottlenecks.
C. Low-Scrap Laser Pattern Nesting and Digital 3D Sampling: The traditional paradigm of producing three to five rounds of physical prototypes across several months is obsolete. Forward-thinking OEM factories leverage 3D simulation software (CLO 3D) alongside automated nesting tables. This reduces fabric waste below 4%, optimizes grainline tension alignment for activewear tights, and cuts prototype development schedules from 45 days down to single-digit turnaround times.
Technical performance sportswear relies heavily on high-tensile yarn innovation. Achieving structural durability without adding bulk or sacrificing moisture transport remains the supreme engineering challenge. Our factory R&D focuses on three primary structural categories:
A. Micro-Denier Interlock & Squat-Proof Knitting: For women's yoga leggings, studio bodysuits, and cross-training apparel, our production incorporates 50-gauge interlock circular knits employing 75D/72F micro-polyamide spun together with genuine Invista Lycra®. This ultra-fine gauge construction achieves complete optical opacity during deep stretching exercises (tested via 180-degree bend stretch sensors) while retaining an airy, weightless hand feel of 210 to 240 GSM.
B. Targeted Zonal Compression and Thermal Regulation: Rather than uniform tightness, modern training shorts, running baselayers, and cycling garments require anatomical pressure mapping. By utilizing variable-tension jacquard structures and laser-perforated back and groin panels, our OEM manufacturing delivers high muscular stability around major quadriceps and hamstrings while facilitating immediate convective cooling across high-perspiration zones.
C. Durable Water Repellent (DWR) C0 Chemistries for Lifestyle Outerwear: The bridge between urban streetwear and tactical athletic outerwear is characterized by midweight windbreakers, running shells, and weather-resistant hybrid tracksuits. In response to global PFAS restrictions, our outerwear facility has completely transitioned to eco-friendly fluorine-free C0 DWR coatings. These hydrophobic treatments bead torrential rainfall up to 10,000mm hydrostatic head pressure while maintaining vapor permeability above 8,000 g/m²/24h.
A systematic, audit-ready engineering protocol ensuring technical tech packs are faithfully translated into mass production without quality loss.
Digital conversion of client design sketches, vector charts, and grading scales. Verification of stretch coefficients, seam allowances, and stress tolerance thresholds prior to cloth consumption.
Yarn procurement from accredited spinners. Computerized spectrophotometer color matching under D65 artificial daylight to guarantee zero delta-E variance across diverse fabric rolls.
Automated vacuum-bed CNC laser cutting ensures millimeter pattern precision. Precision flatlock 4-needle stitching delivers ultra-flat, chafe-free seams capable of withstanding 250N tensile loads.
100% inline seam inspection, dimensional tolerance auditing, needle detection passes, and retail-ready packaging equipped with personalized custom trims, barcodes, and master cartons.
Standard technical specifications across our most frequently sourced athleisure, gymwear, and performance outerwear OEM product categories.
| Garment Category | Primary Textile Composition | Fabric Weight (GSM) | Key Functional Finish | Standard OEM MOQ | Primary Applications |
|---|---|---|---|---|---|
| Seamless Studio Leggings & Tops | 75% Nylon, 25% Spandex (4-Way Interlock) | 220 – 260 GSM | Squat-Proof Opacity Peach Feel | 300 pcs / colorway | Yoga, Pilates, Lifestyle Activewear |
| Marathon & Running Gear | 100% Micro-Filament Polyester or Poly-Elastane | 130 – 160 GSM | Hydrophilic Wicking Quick-Dry | 200 pcs / design | Distance Running, Trail, Marathon Events |
| Sublimated Teamwear Kits | 92% Polyester, 8% Spandex Jacquard Mesh | 150 – 180 GSM | Hi-Definition Sublimation Anti-Snag | 100 sets / team | Soccer, Basketball, Club Tournaments |
| Performance Compression Shorts | 80% Polyamide, 20% Elastane Single Jersey | 200 – 240 GSM | Zonal Elastic Support Antibacterial | 250 pcs / style | Crossfit, Gym Training, Base Layers |
| Technical Windbreakers & Shells | 100% Ripstop Nylon Softshell / Taslan | 110 – 190 GSM | C0 Eco-DWR (10,000mm) Windproof | 200 pcs / style | Outdoor Running, Track Jackets, Streetwear |
| Co-Ord Tracksuit Ensembles | Cotton-Poly Fleece or French Terry Blends | 300 – 380 GSM | Anti-Pilling Treatment Pre-Shrunk | 250 sets / style | Warmups, Travel, Lifestyle Streetwear |
Critical technical, compliance, commercial, and operational queries answered to facilitate rapid supplier onboarding and RFQ evaluation.
Our dedicated internal rapid-sampling facility constructs fully functional prototypes, including custom digital sublimation, lab-dip color matches, and accurate fabric weights, in 7 to 10 working days upon receiving your confirmed tech pack and vector artwork files.
All bulk fabric rolls undergo standardized lab wash tests (AATCC 61 / ISO 105-C06) to ensure Colorfastness Grade 4+ against machine laundering and perspiration. Shrinkage is stabilized below ±3% through pre-shrinkage stenter framing and heat setting prior to garment cutting.
Our baseline OEM MOQ starts at 200 to 300 pieces per style/colorway across standardized performance blends, with multi-size breakdown (XS–3XL). For specialized customized jacquard waistbands or bespoke yarn dye lots, MOQs typically scale to 500 units to ensure fabric mill efficiency.
Yes. 100% of our OEM production is bespoke. We ingest client-supplied CAD blocks, grade rules, bill of materials (BOM), stitch tension specifications, and unique regional fit blocks (US Athletic, European Slim, or Asian Fit) without proprietary lock-in.
We operate according to international ANSI/ASQ Z1.4 (AQL 2.5 Major / 4.0 Minor) protocols. Our internal quality assurance division executes 4-point fabric roll inspections, inline sewing inspections, 100% garment measurement audits, metal detection scanning, and drop-test packaging verification.
We provide comprehensive global trade logistics on FOB (Karachi / Sialkot Dry Port), CIF, and DDP (Delivered Duty Paid) terms via air freight (DHL, FedEx, air cargo consolidators) and ocean container lines for volume freight to major hubs across the USA, UK, EU, and Australasia.
Connect directly with our senior textile engineers and export merchandising team. Submit your technical design brief or schedule an engineering consultation to receive rapid sample development pricing within 24 hours.