
Constructed using high-tenacity nylon-spandex blends, hollow-fiber thermoregulation knit structures, and flatlock anti-friction stitching for professional athletes and commercial brands.
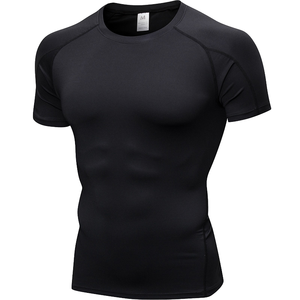
As consumer demand shifts toward hybrid athletic living, performance sports undergarments demand surgical precision across moisture-wicking gradients, elastane recovery, and anti-microbial longevity.
Modern athletic underwear has abandoned single-layer polyester constructions. The leading edge utilizes differential bi-component double-knit weaves: micro-denier hydrophobic synthetic yarns on the inner skin surface repel perspiration immediately, forcing moisture toward hydrophilic outer face fibers for accelerated evaporative dissipation.
By integrating jacquard circular knitting machinery, base layers feature graduated porous mesh zones directly woven into high-heat thermal epicenters—including the lumbar curve, perineal region, and groin. This technique completely eliminates additional seam junctions that traditionally cause athlete chafing and micro-tears.
Export compliance mandates the departure from surface-topical chemical wash finishes that degrade after 10 industrial wash cycles. We implement permanent silver-ion (Ag+) masterbatch extrusions and zinc pyrithione yarn infusion, maintaining 99.4% anti-bacterial pathogen neutralization across 50+ commercial wash life cycles.
A clear breakdown of textile attributes to guide global procurement managers in selecting the ideal textile blend for compression, running, and fitness base layers.
| Material Architecture | Composition Ratio | Tensile Modulus (MPa) | Moisture Vapor Rate (JIS L 1099) | Recommended Use Case |
|---|---|---|---|---|
| Micro-Nylon Tactel 6.6 | 82% Polyamide / 18% Spandex | 12.5 - 14.0 | 8,500 g/m²/24h | Marathon & Long-Distance Run |
| Interlock Poly-Coolmax | 88% Recycled Poly / 12% Elastane | 9.8 - 11.2 | 11,200 g/m²/24h | High-Heat Outdoor Athletics |
| Bamboo-Carbon Hybrid | 65% Bamboo / 28% Poly / 7% Lycra | 7.2 - 8.5 | 7,100 g/m²/24h | Daily Active & Recovery Base |
| High-Compression Warp Knit | 75% Micro-Poly / 25% Creora High-Power | 16.5 - 18.2 | 9,000 g/m²/24h | Strength & Combat Sports Base |
Anticipating buyer behavior shifts, circular supply chain mandates, and digital factory integration across the sports apparel manufacturing sector.
International regulatory pressures—such as the EU Corporate Sustainability Due Diligence Directive (CSDDD)—are propelling wholesale buyers away from virgin crude-derived synthetics. By incorporating chemically recycled GRS-certified post-consumer rPET and ocean plastics, base layers retain pure performance resilience without carbon tax liabilities.
Traditional mechanical sewing is reaching thermal limits. Forward-looking exporters are replacing standard overlock stitches with high-frequency ultrasonic bonding and thermally fused elastic membranes. The outcome: completely stitch-free garments that eliminate bulk, cut aerodynamic drag, and eradicate friction burns during high-impact movement.
Brand inventory risks are mitigated through automated CAD/CAM pattern rendering, 3D Clo cloaking digital samples, and low-waste laser-cutting tables. Global importers now mandate dynamic MOQ scaling alongside synchronized automated bulk production, slashing new design-to-freight cycles down to 30 days.
From raw filament selection to sealed export cartons, every production milestone is governed under stringent international audit benchmarks.
We manage high-density circular knitting, automated cutting, precision flatlock stitching, sublimation, and quality control under one roof—eliminating subcontractor delays, variance, and markup.
Zero toxic heavy metals, formaldehyde, or unregulated azo dyestuffs. Our facility upholds ISO 9001 Quality Management systems with documented lot-by-lot inspection reports ready for commercial customs clearance.
Equipped with specialized R&D pattern engineers, we transform your tech pack or reference sample into market-ready, fit-tested prototypes within 7 to 10 days, accelerating your seasonal go-to-market timetable.
Serving importers across North America, Europe, Australia, and Asia with streamlined FOB, CIF, and DDP trade terms. Complete export customs documentation is coordinated directly by our dedicated logistics team.
Essential operational guidelines covering order parameters, compliance, custom packaging, and sample verification procedures.
Whether you require precision OEM base layers, seamless compression underwear, or full activewear private labeling, our technical engineering team delivers uncompromised consistency from tech pack to global port.
Send an Inquiry