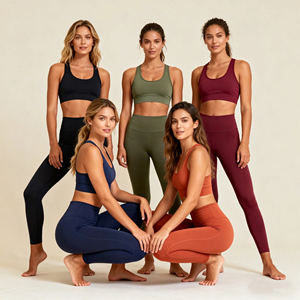
Seamless athletic wear represents the nexus of high-precision circular knitting, polymer science, and anatomical compression mapping. As global procurement shifts toward zero-friction, skin-feel performance apparel, verified tier-one Chinese manufacturing ecosystems provide unprecedented supply stability, proprietary circular yarn compositions, and full vertical integration.
Explore eight core performance silhouettes engineered on advanced Italian Santoni circular knitting machinery, incorporating gradient micro-ribbing, targeted core stabilization, and breathable hollow-fiber nylon compositions.
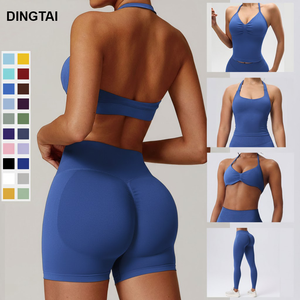
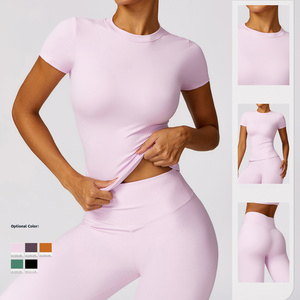
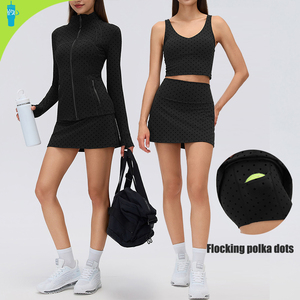
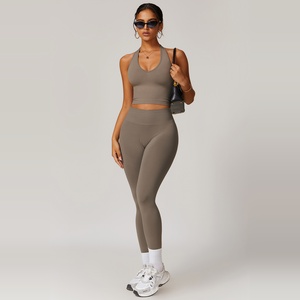
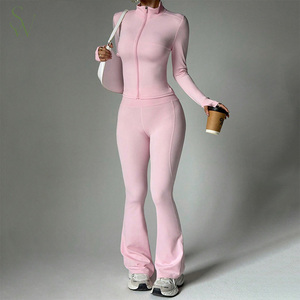
Combining complete in-house circular weaving, computerized pattern grading, eco-conscious package dyeing, and strict multi-checkpoint quality controls to eliminate vendor risks for international retail chains.
Every step from yarn winding, seamless circular knitting, link-stitching, pressure dyeing, heat sublimation, to final laser finishing is held under one managed roof. By eradicating intermediary subcontracting, we guarantee uniform GSM, dimensional consistency, and flawless batch repetition.
With multi-decade cross-border logistics expertise, we supply top retail labels across North America, the UK, Europe, Australia, and Asia-Pacific. We manage full customs documentation, GSP declarations, tariff-code optimization, and transparent FOB, CIF, or DDP consignments.
We transform initial tech packs or CAD sketches into market-ready retail collections. Comprehensive customization supports micro-jacquard knitting of logos, engineered contour shading, custom silicone gripping, bespoke hangtags, and biodegradable branded polybags.
Operating under rigid ISO 9001 certified protocols and working exclusively with OEKO-TEX Standard 100 Class I compliant yarns. We apply 4-point fabric grading, AQL 2.5 final auditing, tensile burst testing, and complete 40-wash colorfastness validation.
Precision computerized scheduling shortens standard counter-sample development to 7–10 working days. Mass seamless batch runs ship within 30–45 days, supported by reserved production pipelines that insulate your brand against seasonal retail spikes.
Eliminate commercial brokers. Our technical merchandising teams consist of senior textile engineers who converse fluently in English, conducting live video technical sessions, digital CAD approvals, and providing high-definition weekly production checkpoint feeds.
Analyzing key structural transformations driving the activewear industry: from flat 2D cut-and-sew apparel to dynamic, graduated compression knitwear engineered for high physical performance and metabolic regulation.
Seamless engineering utilizes computer-governed cylinder needle selection, transitioning tension dynamically across the garment. Leggings incorporate 18-22 mmHg targeted venous support around lower calves while transitioning to low-tension flexible ribbing at the popliteal fossa behind the knees, preventing bunching during deep yoga extensions.
Modern yoga brands require rigorous environmental accountability. The transition away from virgin petroleum nylon toward GRS-certified post-consumer recycled Polyamide 6.6 and plant-derived castor oil bio-polymers ensures circular lifecycle compliance while improving wicking velocity and fabric drape.
By blending variable thread deniers directly during knitting, manufacturers create intricate pointelle mesh structures, dimensional honeycomb motifs, and seamless contour lines. This bypasses the need for abrasive secondary seams, drastically reducing chafing during hot yoga sessions.
| Evaluation Parameter | Traditional Cut & Sew Yoga Wear | High-Gauge Circular Seamless (Advanced China OEM) | Sourcing Benefit |
|---|---|---|---|
| Seam Profile & Friction Points | Multiple overlock/flatlock joining seams across thighs, sides, and waistband. | Zero longitudinal side seams; tubular knit structure with flat-bonded gussets. | Drastic reduction in chafe points; zero pressure points during mat workouts. |
| Fabric Scrap & Material Loss | 18% – 25% cutting waste from standard markers and nested patterns. | Under 2.5% scrap rate; yarn is knitted straight into garment silhouettes. | Direct reduction in raw material expenditure and high ESG brand alignment. |
| Multi-Zone Compression Integration | Requires piecing different fabric weights via bulky interlock seams. | Dynamic stitch variation within a single uninterrupted tubular panel. | Uniform anatomical recovery without structural breakdown or seam failure. |
| Elasticity & Shape Memory | Elastic degradation localized around stress-bearing needle punctures. | Continuous elastane co-knitting with four-way 360-degree modulus return. | Zero bagging around knee and glute zones after repeated commercial wash cycles. |
Global athleisure supply chains are undergoing structural reallocation. Sourcing managers must realign their vendor selection strategies to address changing global requirements, circular design criteria, and regional production clusters.
Procurement directors are shifting from massive single-season purchase orders to continuous, responsive replenishment models. Suppliers in China utilize automated digital knit programming to handle flexible initial runs, allowing brands to test complex colorways and restock bestselling lines within a compressed 20-day timeframe.
Stricter European and American chemical and effluent discharge regulations are driving the adoption of dope-dyed yarns. Color masterbatch is blended directly into the liquid polymer prior to yarn extrusion, cutting wastewater discharge by 80% while achieving superior grade-5 colorfastness against sweat and UV exposure.
Next-generation seamless activewear combines phase-change materials (PCM), micro-encapsulated jade particles, and infrared-emitting bioceramic yarns. These fibers absorb excess thermal radiation during intense workout phases and slowly discharge heat back to muscles during post-exercise recovery.
With incoming EU circularity mandates, seamless yoga brands are implementing raw-material origin tracking via scannable QR tags. Top Chinese production hubs facilitate complete chain-of-custody documentation from raw flake to spun yarn, knitting, finishing, and individual packaging.
Essential operational and technical clarifications addressing minimum order thresholds, machinery setup overhead, shrinkage control, and private labeling.
Seamless knitting runs on circular cylinder machinery that requires precise diameter adjustments per garment size (e.g., 12", 13", 14", 15" cylinders). Setting up needle parameters, thread guides, and running specific yarn dye vats entails significant machinery downtime. Consequently, professional manufacturers typically establish minimum order quantities per color and size run (often 500-1,000 units per colorway) to ensure optimal production efficiency.
In seamless production, fabric weight is not regulated by buying pre-milled fabric rolls. Instead, GSM is governed directly on the loom by modulating yarn tension, feeding speeds, fiber denier (e.g., 40D vs 70D Elastane wrapped with Polyamide), and selecting specialized knit structural designs such as double-jersey, pique, or rib structures within the programming interface.
We perform multi-axis stretch testing under standardized D65 lighting environments. To guarantee opacity in pastel, earth, and light-toned yoga pants, we increase elastane plating density, apply high-filament count air-jet textured nylon (ATY), and use dual-feed knitting patterns. This ensures complete opacity even under maximum bidirectional extension at the glutes.
Seamless tubes exit circular knitting machines in an unrelaxed state. Our vertically integrated facilities subject tubular blanks to computerized continuous pre-shrinking and heat-setting steam chambers prior to cutting and sewing. This thermal stabilization locks fabric memory, limiting downstream domestic washing shrinkage to less than 3% across length and width.
Yes. We can knit your brand emblem, sizing indicators, wash instructions, and custom architectural contours directly into the waistband or interior ribbing using high-density jacquard knitting programs. Alternatively, we provide high-elasticity silicone thermal transfers, reflective PU emblems, and custom metal hardware tags.
Our manufacturing network maintains ISO 9001 certified quality administration and undergoes independent third-party audits (such as BSCI and Sedex SMETA). All fabrics meet OEKO-TEX Standard 100 criteria, ensuring zero hazardous azo dyes, formaldehyde, or heavy metals. Complete third-party inspection certificates and customs clearances are supplied on demand.
Submit your design tech pack, sample reference, or custom fabric requirements. Our technical development team will review structural feasibility, supply swatch lab-dips, and provide transparent volume pricing within 24 hours.