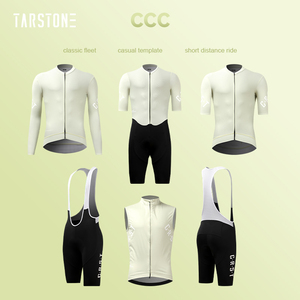
Explore precision-cut gymwear, high-tensile martial arts compression layers, all-weather running gear, and technical cycling garments engineered for international sports brands.
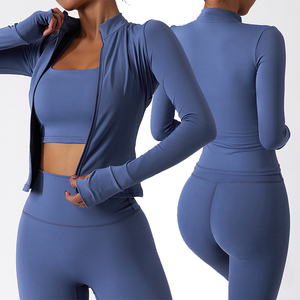

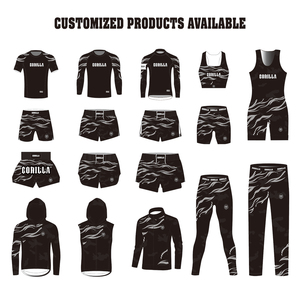
The international sportswear and performance apparel marketplace is undergoing an unprecedented structural evolution. Global brands, disruptive direct-to-consumer (D2C) athletic labels, and fitness chains can no longer rely on simplistic cut-and-sew operations. Modern activewear sourcing demands sophisticated supply chain integration, technical yarn synthesis, digital 3D pattern grading, cleanroom bonding, and stringent sustainability auditing. China's top private label activewear manufacturers represent the epicenter of this technological shift, bridging the gap between raw scientific textile innovation and market-ready performance collections.
Historically, athletic garment procurement revolved primarily around cost-per-unit metrics. Today, search intent data and enterprise procurement behavior reveal that purchasing directors prioritize supply chain velocity, low fabric defect rates (measured under AQL 1.5/2.5 standards), environmental certifications (OEKO-TEX Standard 100, GRS, bluesign®), and intellectual property protection. Chinese activewear hubs—spanning Guangdong, Zhejiang, and Fujian—have evolved from manual assembly facilities into vertically integrated technical laboratories where polymer science, circular recycling, and ultrasonic bonding coalesce.
B2B Strategic Insight: Top-tier Chinese OEM/ODM activewear exporters operate fully unified ecosystems where knitting, dying, laser cutting, automated flatlocking, sublimation printing, and multi-tier quality control function under one roof. This minimizes subcontracting handoffs and reduces defect variances to under 0.8% across bulk runs.
Whether manufacturing high-compression seamless yoga leggings, IBJJF-grade MMA rashguards, or DWR-coated ultra-breathable running shells, premier exporters provide comprehensive tech-pack interpretation and prototyping services. Brands entering multi-million-dollar supply contracts require full traceability back to virgin or recycled yarn extruders, rigorous dye fastness data (ISO 105-C06 Class 4+), and hydrostatic head verification for weather-proof membranes. China's leading private label exporters have adapted to satisfy these institutional compliance standards across North America, Europe, Australia, and the Middle East.
Decades of technical mastery combined with institutional quality controls enable seamless transitions from initial technical design to retail-ready worldwide container shipments.
Eliminate subcontracting volatility. From pattern engineering, automated laser cutting, 4-needle 6-thread flatlocking, to Italian dye-sublimation and silicone heat-sealing, all critical processes are contained within our facilities.
Stringent adherence to international labor, environmental, and toxicity thresholds. Every roll of performance yarn is verified free of harmful aromatic amines, formaldehyde, heavy metals, and per- and polyfluoroalkyl substances (PFAS).
Time-to-market defines athletic apparel profitability. Receive physical prototypes and lab dips within 7 to 10 working days, backed by full 30 to 45-day commercial bulk turnaround cycles for regular high-volume reorders.
Serving over 50 sovereign markets across North America, the EU, UK, GCC, and APAC. We provide seasoned documentation handling under FOB, CIF, DDP, and DDU incoterms, minimizing tariff friction and clearance delays.
Deliver retail-ready, branded activewear straight to your distribution centers. Comprehensive branding options include custom woven neck tags, recycled high-density silicon transfers, branded polybags, and FSC-certified hangtags.
Our dedicated CAD engineering team optimizes ergonomic seam placements, graded European/US/Asian size charts, and differential compression zones to prevent garment ride-up and friction points during high-velocity sports movement.
Anticipating material science advances, circular economy legislation, and automated production shifts shaping athletic garment procurement worldwide.
The activewear sector is pivoting away from virgin petroleum-based synthetics. Enterprise buyers now mandate Global Recycled Standard (GRS) certified rPET derived from ocean-bound plastics, bio-based castor bean polyamides, and chemically recyclable elastane fibers designed for closed-loop textile recovery.
Traditional needle-and-thread stitching is increasingly augmented by ultrasonic bonding and seamless santoni circular knitting. Eliminating raised seams maximizes hydrodynamic/aerodynamic efficiency, prevents skin abrasion during marathon runs, and reduces fabric cut-off waste by up to 35%.
Modern consumers require active cooling and sustained freshness. Factories are integrating micro-encapsulated phase change materials (PCMs) that absorb body heat during exertion, alongside permanent non-migrating silver-ion and zinc-pyrithione antimicrobial finishes resisting over 50 home wash cycles.
Physical sampling iterations are being streamlined through 3D virtual fitting simulations. By applying accurate tension maps, drape parameters, and dynamic avatar movement tests in Clo3D, tech-pack approval times drop from 30 days to under 7 days, conserving both fabric capital and developmental budgets.
With EU Corporate Sustainability Due Diligence Directives (CSDDD) taking effect, exporters are embedding QR-enabled Digital Product Passports (DPP). These provide verified data covering tier-1 to tier-4 carbon footprints, water consumption metrics during dyeing, and chemical safety documentation.
The boundaries separating performance sportswear from everyday casualwear have dissolved. Modern procurement heavily features heavyweight boxy cotton-elastane blends, matte-finish nylon interlocks, and covert technical features like hidden zip pockets that transition seamlessly from intensive gym training to executive spaces.
Institutional comparison of performance properties, weight distributions, and targeted athletic disciplines across core export materials.
| Fabric Specification | Composition & Yarn Count | Weight (GSM) | Moisture / Air Permeability | Key Athletic Applications | Testing Standard |
|---|---|---|---|---|---|
| Butter-Soft Nude Feel | 75% Nylon 6.6 / 25% Spandex (40D+40D) | 220–250 GSM | Wicking Rate < 1.5s, 4-Way Stretch > 180% | Yoga Leggings, Sports Bras, Pilates Sets | AATCC 79 / 197 |
| High-Tenacity Combat Knit | 85% Recycled Poly / 15% Elastane | 240–280 GSM | Burst Strength > 420 kPa, Anti-Tear | BJJ Rashguards, MMA Fightwear, Grappling | ASTM D3787 |
| Aerodynamic Marathon Mesh | 100% Quick-Dry Micro-Polyester | 110–135 GSM | Air Permeability > 180 cm³/cm²/s | Marathon Singlets, Track Racing Tops | ASTM D737 |
| DWR Weatherproof Shell | 100% Ripstop Nylon + Breathable PU | 90–120 GSM | 10,000mm Hydrostatic / 8,000g/m²/24hr | Running Jackets, Windbreakers, Trailwear | JIS L1092 / L1099 |
| Heavyweight Urban Boxy Knit | 95% Combed Compact Cotton / 5% Elastane | 260–300 GSM | Colorfastness to Washing: Grade 4.5 | Oversized Training Tees, Street Gym Hoodies | ISO 105-C06 |
| Italian High-Gauge Chamois Mesh | 80% Polyamide / 20% Elastane Aeromesh | 180–210 GSM | UPF 50+ Sun Protection, High Recovery | Cycling Bib Shorts, Team Jersey Kits | AS/NZS 4399 |
Addressing essential technical queries, minimum order quantities, compliance protocols, and production variables for professional procurement officers.
Our standard MOQ is tiered depending on custom fabric dyeing requirements. For stock color fabrics with custom screen printing, sublimation, or silicone transfers, our baseline is 100 to 200 pieces per design/color across mixed sizing (XS–3XL). For custom pantone yarn-dyeing or specialized technical fabric developments (such as proprietary recycled nylon-spandex blends), the typical MOQ is 500 to 1,000 pieces per colorway.
Every inbound fabric lot undergoes strict lab verification prior to spreading and cutting. We test squat-proof opacity using digital photometric sensors under 85% tensile elongation. Colorfastness to perspiration (ISO 105-E04) and rub crocking (AATCC 8) must meet or exceed Grade 4. Seam elasticity is secured using genuine 4-needle 6-thread flatlock machines calibrating stitch tension to withstand >180% fabric elongation without stitch rupture.
Our standard production workflow is structured into clear, milestone-driven phases: Prototyping, pattern grading, and physical sample fabrication require 7 to 10 working days. Once the pre-production (PP) sample receives formal client sign-off, commercial bulk manufacturing requires 30 to 45 calendar days depending on total order volume and complexity. Air express delivery requires 3–5 days, while ocean shipping to North America or Europe takes 18–28 days.
Yes. We maintain active compliance and sourcing partnerships with certified yarn processors providing Global Recycled Standard (GRS) and OEKO-TEX Standard 100 Class 1 fabrics. We furnish official Transaction Certificates (TCs) with bulk export orders, verifying the provenance of post-consumer recycled polyester (rPET) or post-industrial regenerated nylon (ECONYL® compatible) directly to regulatory bodies and customs authorities.
We enforce a standard 4-stage internal QA regimen: Inbound raw fabric inspection (4-Point System), in-line sewing checks at every workstation, semi-finished garment inspection, and final AQL 1.5/2.5 random sampling before boxing. We actively welcome third-party international inspection agencies (such as SGS, Intertek, Bureau Veritas, or QIMA) to inspect lots at our facility before final balance payment and container sealing.
Intellectual property protection is a core corporate tenet. Prior to receiving any customer vector files, sizing specifications, or brand artwork, we routinely execute bilateral Non-Disclosure Agreements (NDAs). Custom prints, sublimation artwork, proprietary silicone embossings, and private label trims are maintained under secure access-controlled servers and are never resold or displayed to third parties.
Whether you are scaling an established athletic apparel brand, outfitting a global marathon series, or engineering high-performance combat gear, our senior merchandising and pattern-engineering team is standing by to analyze your tech packs.