
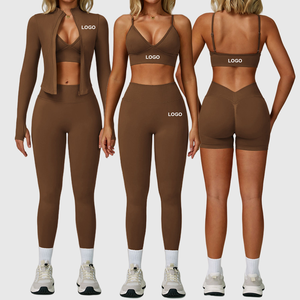
From high-density brushed fleece training pullovers to seamless compression wear and fully customized athletic uniforms, explore our core manufacturing capabilities built for global apparel brands.
A comprehensive technical examination of industrial knitting, heavy-density fleece processing, seam stabilization, and supply chain governance for enterprise procurement teams.
In high-intensity training and premium lifestyle athleisure, a gym hoodie must deliver thermodynamic regulation, anti-pilling longevity, ergonomic freedom, and structural weight. As a preeminent fleece gym hoodie manufacturer, our factory deploys double-knit, three-end fleece (3-End French Terry & Polar Fleece) knitting structures that isolate yarn functions:
Procurement directors must balance seasonal adaptability against retail weight perception. We manufacture across specialized weight thresholds:
Athletic hoodies fail most frequently under cyclic tensile loading along shoulder yokes, underarm seams, and pocket anchors. Our automated cutting and stitching lines incorporate structural engineering safeguards:
| Enterprise Fleece Gym Hoodie Technical Specifications | |
|---|---|
| Available Fabric Compositions | 100% Combed Compact Cotton, 80/20 Cotton-Poly CVC, 65/35 Poly-Cotton TC, 95/5 Cotton-Elastane, Recycled GRS-Certified Polyester Fleeces |
| Fabric Weight Range | 280 GSM, 320 GSM, 360 GSM, 420 GSM, 480 GSM, and custom heavyweight 550 GSM loopback knits |
| Dyeing & Color Fastness | Reactive piece dyeing, garment pigment vintage wash, acid wash; Grade 4-5 fastness to laundering, rubbing, and perspirative staining (ISO 105-C06) |
| Embellishment Technologies | High-density silicone heat transfers, 3D puff embroidery, discharge screen printing, laser-cut appliqué, Chenille patches, metal-tipped custom drawcords |
| Quality & Testing Audits | Inline 4-point inspection system, automated fabric inspection machines, metal detector needle check, OEKO-TEX Standard 100, ISO 9001 certified |
| Production Lead Times | Rapid proto/fit sampling in 7–10 days; bulk manufacturing turnaround within 30–45 days post-approval |
How global market shifts, raw material innovations, and digital supply chain integration are redefining commercial garment contracts for forward-thinking sportswear brands.
Procurement mandates across North America and the EU increasingly require Global Recycled Standard (GRS) certification. Leading sportswear brands are migrating toward rPET/organic cotton fleece blends and water-saving closed-loop dyeing processes that reduce carbon footprints by up to 34% per garment batch.
The boundary between traditional cotton gym hoodies and technical outerwear is evaporating. Future sourcing lines focus on bonded composite fleece: an abrasion-resistant stretch woven exterior bonded with a micro-fleece thermal backing via a breathable polyurethane (PU) membrane for windproof outdoor training.
To mitigate deadstock inventory liabilities, global buyers are pairing initial core seasonal buys with responsive short-run replenishment contracts. Vertical factories that store greige fleece fabric ready for rapid reactive piece dyeing allow brands to replenish best-selling SKUs within 15 to 20 days.
From silhouette engineering to yarn level biostatic treatments, observe the structural paradigm shifts driving modern athletic pullover development.
Heavy gym sweat retained in traditional thick fleece fosters bacterial colonies, producing persistent odors. Modern technical fleece fabrics incorporate silver-ion or zinc-pyrithione polymer additions at the extrusion phase, inhibiting odor-causing bacteria across the garment's operational lifespan.
Athletes reject restrictive traditional slim-cut designs in favor of vintage-inspired boxy fits with extended chest circumferences and forward-rotated shoulder seams. This cut provides complete range of motion during bench presses and squats while providing a tailored retail aesthetic.
Modern lifters demand seamless integration for smartphones, wireless audio charging cases, and lifting straps. New construction patents feature invisible internal zip compartments hidden within the front kangaroo pocket, audio cable pass-throughs, and reinforced thumbholes in double-ply cuff systems.
Our vertically integrated production ecosystem eliminates middleman markups, reduces sample iteration delays, and guarantees ISO 9001 quality compliance across every exported container.
Knitting, precision fabric cutting, automated stitching, screen printing, embroidery, sublimation, and final quality packaging occur under one roof. Centralized processing removes subcontractor delays and guarantees seamless lot-to-lot color matching.
Exporting high-volume apparel shipments to the USA, UK, Germany, France, Canada, and Australia on FOB, CIF, or DDP terms. Our dedicated logistics export desk manages customs manifests, HS code classifications, and import documentation seamlessly.
We transform your digital CAD tech packs or physical benchmark samples into fully customized collections. Includes branded woven neck labels, silicone transfers, debossed eyelets, customized aglets, barcode hangtags, and frosted polybag packaging.
Our operations follow rigid ISO 9001 quality management procedures. Every dye lot is rigorously screened for hazardous aromatic amines, formaldehyde, and heavy metals, meeting full OEKO-TEX Standard 100 and REACH environmental compliance.
Time-to-market determines athleisure brand success. Our dedicated R&D pattern workshop completes initial fit prototypes in 7 to 10 working days, backed by automated bulk production schedules completed in 30 to 45 days.
Work directly with seasoned textile engineers and export merchandisers who understand Western sizing standards, AQL 2.5 acceptance quality limits, and international retail delivery deadlines—avoiding third-party miscommunication.
Clear, direct operational answers to technical specifications, minimum order quantities, compliance documentation, and global export shipping terms.
Our standard production MOQ is typically 100 to 200 units per colorway and design, supporting multiple size gradations (XS to 3XL). For custom-knitted specialized fabric weights, unique yarn blends, or custom reactive pantone dye baths, typical minimums start around 300 to 500 units per color. We offer flexible trial volume tiers for emerging high-growth athletic labels.
Pre-production fit and proto samples are finalized within 7 to 10 working days upon tech pack receipt and fabric confirmation. Once sample measurements, fits, and print strike-offs are approved, bulk production takes 30 to 45 calendar days depending on decoration complexity, order volume, and packaging configurations.
All knitted fleece rolls undergo pre-shrinking, high-temperature stenter heat-setting, and compacting prior to pattern cutting. We ensure dimensional stability within a rigorous <3% shrinkage tolerance (AATCC 135) and a Grade 4 colorfastness rating under continuous industrial wash conditions.
Yes, 100% of our production supports bespoke OEM/ODM private label specifications. We develop full collections from your Adobe Illustrator tech packs or reference samples, integrating customized woven labels, silicone branding badges, heat-sealed care labels, laser-engraved eyelets, customized aglets, and retail packaging ready for immediate e-commerce distribution.
Our facility operates under ISO 9001 quality management systems and maintains full compliance with OEKO-TEX Standard 100 Class I & II fabrics, GRS (Global Recycled Standard), and BSCI social compliance guidelines. We provide accredited third-party test reports (SGS, Intertek, or TÜV) upon buyer request covering tensile strength, pilling resistance, and chemical safety.
We routinely execute commercial shipments under FOB (Shanghai / Ningbo / Qingdao / Karachi), CIF, CFR, and DDP (Delivered Duty Paid) arrangements directly to your brand's distribution centers across the United States, United Kingdom, European Union, Canada, Australia, and the Middle East.